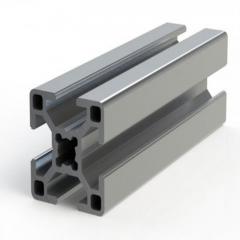
Ever tried cutting aluminum extrusion only to end up with gummed-up blades, jagged edges, or cuts so crooked they're unusable? You're not alone. Whether you're building a 3D printer frame, assembling custom furniture, or fabricating industrial components, finding the best way to cut aluminum extrusion can feel like navigating a maze of conflicting advice scattered across dozens of forum threads.
Here's the problem: aluminum's unique properties make it deceptively tricky to cut cleanly. Its softness causes material to melt and stick to blade teeth. Its ductility creates stubborn burrs that require extra finishing work. And using the wrong tool or technique? That's a recipe for dangerous kickback, wasted material, and frustration that makes you want to abandon your project entirely.
Unlike steel or wood, aluminum extrusion requires a delicate balance of speed, blade selection, and technique. The material's high thermal conductivity means heat builds up quickly during cutting. Too slow, and the aluminum gums onto your blade. Too fast, and you risk melting the material or creating rough, chipped edges.
Common extrusion alloys add another layer of complexity. The popular 6061 alloy used in structural applications cuts differently than 6063, which dominates architectural profiles. Understanding how to cut aluminum extrusion properly means matching your method to both the alloy and profile type—whether you're working with solid bar stock, hollow tubes, or complex T-slot designs.
Professional machinists have solved these challenges, but their solutions often require industrial equipment most hobbyists don't own. Meanwhile, DIY forums offer creative workarounds, but separating proven techniques from well-intentioned guesses takes hours of research. Learning how to cut aluminium effectively shouldn't require sifting through hundreds of posts to find what actually works.
This guide bridges the gap between professional cutting guides and hobbyist forum discussions. We've consolidated real-world user experiences with professional techniques to create a definitive, ranked comparison of cutting aluminum extrusion methods.
You'll find method-by-method breakdowns covering:
Each method includes clear rankings for different scenarios: hobbyist projects, production runs, and budget-conscious builds. You'll learn which blade specifications actually matter, why cutting speed can make or break your results, and how to troubleshoot common problems like burr formation and blade gumming.
Ready to finally get clean, precise cuts on your aluminum extrusion projects? Let's dive into the evaluation criteria that separate good cuts from great ones.
Not all cutting methods are created equal—and the "best" choice depends entirely on your specific situation. A technique that delivers flawless results on solid bar stock might crush thin-wall tubing. A saw to cut aluminum that excels in a professional shop could be overkill for occasional hobbyist projects. That's why we developed a comprehensive ranking system that accounts for real-world variables most guides overlook.
Rather than relying solely on manufacturer specifications, our rankings incorporate feedback from machinists, fabricators, and DIY enthusiasts who work with aluminum extrusion daily. We evaluated each cutting method against the same criteria, weighting factors based on what matters most for different user scenarios.
Here's what we measured:
When cutting aluminum, two variables dramatically influence your results: the alloy you're working with and the profile's complexity.
Consider alloy differences first. According to Triad Products, 6063 aluminum—often called architectural aluminum—offers excellent extrudability and superior surface finish but lower tensile strength. This softer alloy is more prone to gumming during aluminium cutting if you use incorrect speeds. Meanwhile, 6061 aluminum provides greater tensile strength and better machinability, making it more forgiving during saw cutting aluminum operations. However, 6061's increased hardness means faster blade wear.
| Property | 6061 Aluminum | 6063 Aluminum |
|---|---|---|
| Common Applications | Structural components, frames | Architectural profiles, window frames |
| Machinability | Good | Fair |
| Surface Quality | Fair | Great |
| Cutting Behavior | More forgiving, cleaner chips | Softer, higher gumming risk |
| Blade Wear Impact | Higher wear rate | Lower wear rate |
Profile complexity influences tool selection just as significantly. Solid bar stock handles aggressive cutting methods well—the material mass absorbs vibration and dissipates heat effectively. Thin-wall hollow sections tell a different story entirely. These profiles can deform, chatter, or collapse under cutting pressure if you choose the wrong approach.
T-slot extrusions present their own challenges. The internal webbing and multiple wall thicknesses mean the blade encounters varying resistance throughout each cut. Methods that work beautifully on simple rectangular tubing may produce inconsistent results on complex T-slot designs.
Understanding these variables helps you interpret our rankings accurately. A method earning top marks for solid profiles might rank lower for hollow sections—and that's precisely the nuance missing from most cutting guides. With these criteria established, let's examine the top-ranked method that delivers clean results for the widest range of users.
Can you cut aluminum with a miter saw? Absolutely—and for most users, it's the single best method available. The miter saw combines precision, repeatability, and accessibility in ways other tools simply can't match. Whether you're fabricating a 3D printer enclosure or assembling industrial frames, cutting aluminum with miter saw equipment delivers consistently clean results once you understand the critical details.
But here's where most people go wrong: they treat aluminum like wood and grab whatever blade happens to be installed. That approach guarantees frustration. Success with an aluminum cutting miter saw setup depends almost entirely on blade selection and speed management. Get these right, and you'll wonder why you ever struggled with aluminum cuts.
What makes miter saws the top-ranked choice for cutting aluminum extrusion? Several factors combine to create an ideal cutting environment:
Can I cut aluminum with a miter saw if I've never done it before? Yes—the learning curve is surprisingly gentle compared to circular saws or band saws. The fixed cutting geometry removes variables that trip up beginners, letting you focus on proper clamping and feed rate rather than fighting to maintain a straight line.
Your blade choice matters more than any other variable when cutting aluminum on miter saw equipment. According to ToolGuyd's blade testing, non-ferrous metal blades with TCG (Triple Chip Grind) tooth geometry outperform standard ATB (Alternate Top Bevel) designs by a significant margin.
Why TCG geometry? The alternating flat and chamfered teeth create a shearing action that slices through aluminum cleanly rather than tearing it. ATB blades designed for wood tend to grab aluminum aggressively, causing rough edges and dangerous binding. For the best miter saw blade to cut aluminum, look for these specifications:
Brands like Freud and Diablo consistently receive praise in community discussions. The Freud LU77M010 specifically earns recommendations for cutting non-ferrous tubing and profiles up to 1/4" wall thickness.
| Tooth Count (10" Blade) | Cut Quality | Best Applications | Trade-offs |
|---|---|---|---|
| 60 Teeth | Good | Thick solid profiles, rough cuts needing finishing | Faster cutting, more burr formation |
| 80 Teeth | Very Good | General purpose, T-slot extrusions, most projects | Balanced speed and finish quality |
| 100+ Teeth | Excellent | Thin-wall tubing, visible joints, precision work | Slower feed rate required, higher cost |
For most users, an 80-tooth blade hits the sweet spot between cut quality and versatility. Reserve 100+ tooth blades for applications where edge finish truly matters—visible joints, precision assemblies, or thin-wall profiles prone to chipping.
Even the perfect blade fails if you ignore speed management. Aluminum's thermal conductivity creates a paradox: cut too fast and friction melts the material onto your blade teeth; cut too slow and heat builds up, causing the same gumming problem.
Most 10" miter saws operate around 3,800 RPM—acceptable for aluminum but not ideal. According to SinoExtrud's cutting guide, the optimal range falls between 3,000-4,500 RPM for aluminum extrusion. If your saw offers variable speed, dial it toward the lower end of this range.
Feed rate—how quickly you push the blade through the material—matters equally:
A practical tip that dramatically extends blade life: apply a wax stick to the spinning blade before cutting. This simple lubrication reduces friction and prevents chip welding. For bulk cutting sessions, clean your blade every 20-30 cuts to remove aluminum buildup that degrades performance.
For hobbyists building frames, makers assembling CNC machines, or professionals cutting moderate quantities of extrusion, the miter saw earns its top ranking. The combination of precision, accessibility, and consistent results makes it the go-to choice—provided you invest in the right blade and respect aluminum's unique cutting requirements.
But what if you're working with longer stock that won't fit a miter saw's capacity? That's where circular saws enter the picture, offering versatility that miter saws can't match.
What happens when your aluminum extrusion stock is too long for a miter saw's throat capacity? Or when you need to make cuts on a job site without hauling stationary equipment? That's when cutting aluminum with a circular saw becomes your best friend. This versatile runner-up method trades some precision for portability and flexibility that miter saws simply can't offer.
Here's the reality: a circular saw for cutting aluminum won't deliver the same out-of-the-box accuracy as a miter saw. But with proper technique and setup, you can achieve professional-quality results on stock lengths that would be impossible to handle otherwise. The key lies in understanding what makes aluminum cutting different from the wood-cutting tasks these saws typically handle.
When does cutting aluminum with a circular saw make more sense than using a miter saw? Several scenarios tip the balance:
The trade-off? You sacrifice the built-in precision features that make miter saws so beginner-friendly. Circular saws demand more from the operator—proper clamping, careful alignment, and steady hand control throughout each cut.
Success when cutting aluminum with circular saw equipment depends almost entirely on your setup. Unlike miter saws with their fixed fences, circular saws require you to create the guidance system yourself.
Clamping is non-negotiable. Aluminum extrusion must be secured firmly to prevent movement during cutting. Use at least two clamps positioned on both sides of your cut line—never rely on holding the workpiece by hand. For hollow profiles, place clamps close to the cut to minimize vibration that causes chatter marks.
Guide rails transform accuracy. A straightedge clamped parallel to your cut line provides the reference your circular saw needs. Commercial track saw systems work beautifully, but even a straight aluminum angle clamped to your workpiece dramatically improves results. Position the guide so your saw's base plate rides against it throughout the entire cut.
Support the full length. Long extrusions need support on both sides of the cut. Unsupported material droops during cutting, binding the blade and causing dangerous kickback. Sawhorses, roller stands, or helper hands prevent this problem—never let the cut-off piece fall freely.
Mind the blade guard. Aluminum chips behave differently than sawdust. They're hot, sharp, and prone to jamming blade guards. Clear chips frequently during extended cutting sessions, and verify your guard retracts and returns smoothly before each cut.
Many users wonder about cutting aluminum with skill saw equipment—the lightweight, worm-drive, or sidewinder saws commonly found in woodworking shops. Can these tools handle aluminum extrusion effectively?
The short answer: yes, with important caveats.
Standard skill saws typically spin between 5,000-6,000 RPM—significantly faster than the 3,000-4,500 RPM ideal range for aluminum. This higher speed increases heat generation and gumming risk. You can compensate by:
Dedicated metal-cutting circular saws offer advantages worth considering for regular aluminum work. These tools feature lower RPM motors (around 3,500 RPM), chip collection systems designed for metal shavings, and blade guards that handle metal chips without jamming. If you cut aluminum with circular saw equipment frequently, the investment pays dividends in cleaner cuts and longer blade life.
Blade selection mirrors the miter saw recommendations: TCG tooth geometry, 60-80 tooth count for general work, and carbide tips rated for non-ferrous metals. The Diablo and Freud blades that excel in miter saws perform equally well in circular saws—just verify the arbor size matches your tool.
For users who need flexibility above all else, circular saws earn their runner-up position. They won't match a miter saw's precision without careful setup, but they go places miter saws can't and handle stock sizes that would otherwise require professional cutting services. Master the technique, invest in proper blades, and you'll find cutting aluminium with circular saw equipment surprisingly satisfying.
But what about those delicate hollow profiles and thin-wall tubing that challenge even careful circular saw work? That's where band saws claim their territory—offering gentle, controlled cuts that prevent the deformation other methods risk.
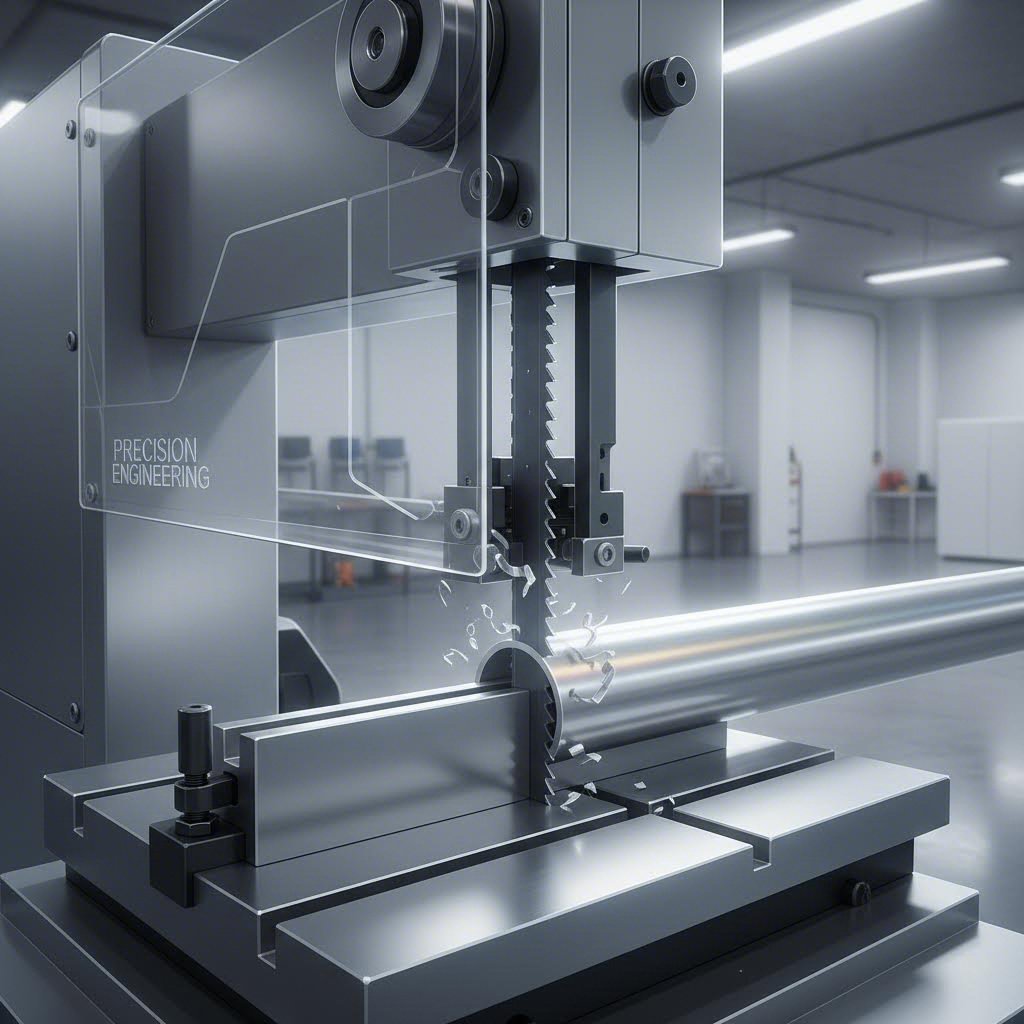
Ever tried cutting thin-wall aluminum tubing with a miter saw only to watch it vibrate, chatter, or crush under the blade's aggressive entry? You're experiencing exactly why band saws claim the precision crown for complex profiles. When you need to band saw cut aluminum without risking deformation, this method delivers control that spinning circular blades simply cannot match.
The secret lies in the cutting action itself. Unlike miter and circular saws that force material through a rotating blade at high speed, band saws use a continuous loop moving in one direction. This creates a pulling action that holds the workpiece steady rather than pushing against it—a critical advantage when working with hollow extrusions and delicate thin-wall sections.
Why do professional fabrication shops rely on band saws for cutting aluminum tubing and complex extrusion profiles? Several mechanical advantages combine to create superior results:
When learning how to cut aluminum tubing without crushing or distorting delicate profiles, band saws solve problems other methods create. The controlled feed rate lets you match cutting pressure to wall thickness—gentle passes for thin sections, more aggressive feeds for solid stock.
Industrial applications reinforce this advantage. Aerospace manufacturers, automotive suppliers, and precision fabricators standardize on band saws for cutting aluminium tube stock precisely because the method preserves dimensional accuracy that downstream processes require.
Choosing the right blade transforms band saw results from acceptable to exceptional. Two specifications matter most: teeth per inch (TPI) and blade material composition.
TPI recommendations for aluminum:
The rule of thumb? Maintain at least three teeth in contact with the material at all times. Fewer teeth cause rough cuts and blade wandering; too many teeth clog with chips and generate excessive heat.
Blade material matters equally. Bi-metal blades—featuring high-speed steel teeth welded to a flexible carbon steel back—outperform standard carbon blades dramatically. The harder tooth tips stay sharp longer when cutting aluminum, while the flexible backing absorbs vibration and resists fatigue cracking during continuous use.
For anyone serious about how to cut aluminium tube stock regularly, investing in quality bi-metal blades pays dividends through extended service life and consistently cleaner edges.
Band saws claim clear superiority in specific scenarios where other methods struggle or fail outright:
The trade-off? Speed. Band saws cut significantly slower than miter or circular saws—a single cut taking 30 seconds on a miter saw might require two minutes on a band saw. For high-volume work with robust profiles, this time difference adds up. But when edge quality and dimensional preservation matter more than speed, the investment in time delivers superior results.
For makers working with delicate aluminum tubing or complex multi-wall extrusions, band saws earn their reputation as the precision specialist. The slower pace becomes irrelevant when you're producing clean edges without the deburring headaches other methods create. But what if your budget doesn't stretch to specialized equipment? Next, we'll explore chop saws and hacksaws—options that get the job done when cost matters most.
Not everyone has $300 to drop on a quality miter saw or space for a band saw in their garage. Sometimes you need to cut aluminum extrusion with whatever tools you already own—or can afford without breaking the bank. That's where chop saws and hacksaws enter the conversation. But here's the honest truth: these budget options come with significant trade-offs you need to understand before committing.
Can you cut aluminum with a chop saw or hacksaw? Technically, yes. Should you expect the same results as purpose-built aluminum cutting methods? Absolutely not. Let's examine when these budget approaches make sense—and when they'll waste your time and materials.
Cutting aluminum with chop saw equipment sounds logical. After all, these machines power through steel rebar and angle iron effortlessly. Aluminum should be easier, right?
Unfortunately, the opposite is true. Most abrasive chop saws create more problems with aluminum than they solve. Here's why:
Can you cut aluminum with a chop saw successfully? Only if you swap the abrasive wheel for a proper carbide-tipped blade designed for non-ferrous metals. This transforms the tool into something resembling a metal-cutting miter saw—though typically with less precision due to looser tolerances in chop saw construction.
If you already own a chop saw and want to try cutting aluminum on chop saw equipment, invest $40-60 in a quality TCG aluminum blade before your first cut. Using the stock abrasive wheel guarantees frustration and potentially dangerous results.
Can you cut aluminum with hacksaw equipment? This question floods DIY forums, and the answer depends entirely on your expectations. A hacksaw costs under $20, requires no electricity, and produces zero risk of blade gumming or melting. For certain situations, these advantages matter more than speed.
Hacksaws work acceptably when:
The practical reality? Cutting even a small T-slot extrusion with a hacksaw takes 3-5 minutes of steady effort. Multiply that by the 20-40 cuts a typical frame project requires, and you've invested hours of arm-burning labor that a miter saw would complete in minutes.
The corner plate workaround: Forum veterans share a practical tip for hacksaw users—don't stress about perfect squareness during cutting. Instead, cut slightly long, then use aluminum corner plates or brackets during assembly to force your joints square. The mechanical fasteners pull components into alignment despite imperfect cut angles. This approach works surprisingly well for 80/20-style framing projects where corner brackets are already part of the design.
For blade selection, choose 24 TPI (teeth per inch) bi-metal hacksaw blades. Finer teeth produce smoother cuts in aluminum's soft material, while bi-metal construction resists the premature dulling that plagues standard carbon steel blades.
Here's the uncomfortable truth that forum discussions often reach after pages of debate: if you need more than a handful of cuts, buying a budget miter saw or using professional cutting services almost always makes more sense than struggling with chop saws or hacksaws.
A basic 10-inch miter saw costs $120-150 new. Add a $50 aluminum blade, and you're cutting cleaner, faster, and more accurately than any aluminum chop saw or hacksaw setup. For projects requiring 20+ cuts, the time savings alone justify the investment.
Alternatively, many aluminum extrusion suppliers offer cutting services at $1-3 per cut. A 30-piece frame project might cost $30-60 in cutting fees—less than the frustration value of hand-cutting that quantity with a hacksaw, and competitive with budget tool purchases you'd need to store afterward.
The budget-conscious approach that actually works? Assess your project scope honestly. One-time projects with few cuts can tolerate hacksaw limitations. Ongoing builds or larger projects warrant proper tooling. And when precision matters more than cost, professional CNC cutting services deliver results no budget tool can match—which brings us to our next method.
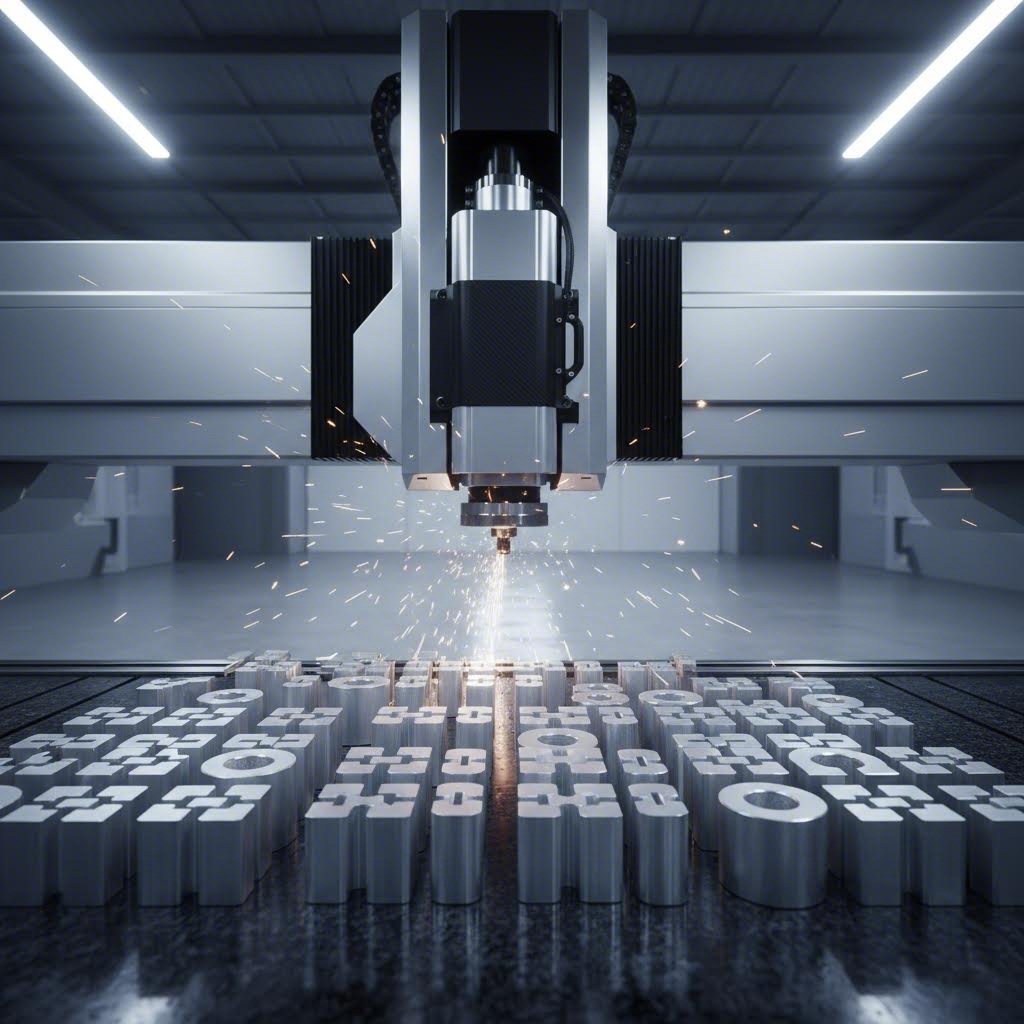
What if the best way to cut aluminum extrusion is... not cutting it yourself at all? For many users, professional CNC cutting services represent the smartest choice—delivering precision that DIY methods struggle to match while eliminating the equipment investment, learning curve, and cleanup headaches entirely.
This isn't about lacking skills or being lazy. It's about recognizing when outsourcing makes financial and practical sense. Professional fabricators with dedicated aluminum extrusion saw equipment and CNC machining centers produce results that even experienced hobbyists admire. Understanding when to leverage these services separates strategic makers from those who waste weekends fighting equipment limitations.
DIY cutting makes sense for many projects—but not all of them. Consider professional cutting services when your situation matches these scenarios:
The math often surprises people. Consider a project requiring 40 cuts on square aluminum extrusion profiles. DIY cutting involves equipment cost (or rental), blade wear, setup time, actual cutting time, deburring, and cleanup. Professional services deliver ready-to-assemble pieces—often for less than you'd spend on a quality blade alone.
Ordering pre-cut extrusions from manufacturers or dedicated fabricators delivers advantages beyond mere convenience:
Factory-direct suppliers operating their own aluminium extrusion line offer particular advantages. These manufacturers control the entire process from die design through final cutting, ensuring compatibility between profile specifications and cutting parameters. Small aluminum extrusions with thin walls especially benefit from this integrated approach, as manufacturers understand exactly how their specific alloys and profiles behave under cutting operations.
Modern CNC machining centers represent the pinnacle of aluminum cutting technology. These computer-controlled systems achieve precision impossible with manual methods:
For users requiring comprehensive aluminum processing, Shengxin Aluminium's deep processing services exemplify what factory-direct CNC capabilities offer. With over 30 years of industry experience and state-of-the-art CNC machining centers, they provide precise cutting, drilling, and bending to exact specifications. Their facility houses 35 extrusion presses ranging from 600T to 5500T, enabling end-to-end support from die development through mass production—a particular advantage for users needing custom profiles cut to specification rather than adapting designs to available stock.
| Factor | DIY Cutting | Professional CNC Services |
|---|---|---|
| Cost per Cut (estimated) | $0.50-2.00 (blade wear + time) | $1.00-3.00 |
| Precision Achievable | ±1-2mm typical | ±0.05-0.1mm typical |
| Time Investment | Setup + cutting + cleanup | Order placement only |
| Equipment Needed | $150-500+ saw, $40-80 blade | None |
| Skill Level Required | Moderate to high | None |
| Burr Cleanup Required | Usually yes | Rarely |
| Best For | Ongoing projects, immediate needs | High volume, tight tolerances, complex cuts |
The comparison reveals an important truth: professional cutting isn't always more expensive when you factor in hidden DIY costs. Equipment depreciation, blade replacement, time value, and material waste from learning-curve mistakes add up quickly. For projects exceeding 20-30 cuts or requiring precision beyond hobbyist equipment capabilities, professional services often represent the genuinely best way to cut aluminum extrusion.
For makers building production quantities, engineers requiring tight tolerances, or anyone lacking workshop space and equipment, professional CNC cutting services earn legitimate consideration as the optimal approach. The question isn't whether you can cut aluminum yourself—it's whether doing so represents the best use of your time and resources.
Of course, whether you cut aluminum yourself or receive professionally processed pieces, problems can still arise. Understanding how to troubleshoot common cutting issues helps you achieve better DIY results and communicate more effectively with service providers when specifications aren't met.
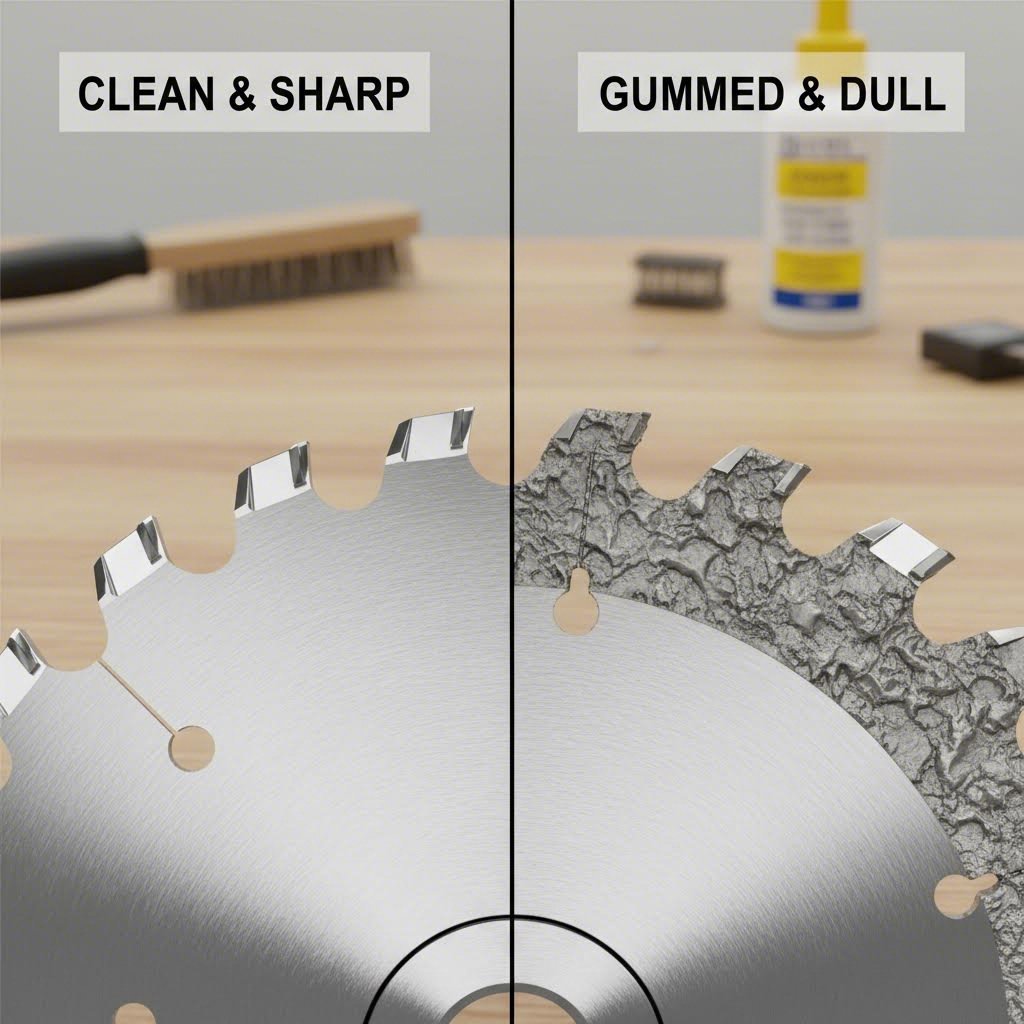
You've selected the right saw, installed a proper blade, and the recommended technique—yet your cuts still aren't coming out clean. Sound familiar? Even experienced fabricators encounter stubborn issues when cutting aluminum extrusion. The difference between frustration and success often comes down to diagnosing problems correctly and applying targeted fixes.
This troubleshooting guide addresses the challenges most guides ignore: the real-world problems that emerge when theory meets workshop reality. Whether you're dealing with jagged burrs, blade gumming, or mysterious chipping, you'll find specific remedies that actually work.
Burrs rank as the most common complaint when learning how to cut aluminum. These raised metal edges form when the blade pushes material aside rather than shearing it cleanly—and they're more than just annoying. Sharp burrs cause assembly problems, create safety hazards, and look unprofessional on finished projects.
What causes burrs to form?
How to eliminate burrs:
Few problems frustrate aluminum cutters more than gumming—that sticky buildup of melted aluminum welded to your blade teeth. Once gumming starts, cut quality deteriorates rapidly. The blade runs hotter, cuts rougher, and eventually stops cutting effectively altogether.
Understanding the cause reveals the solution. Aluminum's low melting point (around 1,220°F) combined with high thermal conductivity means friction heat concentrates at the cutting edge. When teeth move too slowly through material, or when chips aren't cleared efficiently, that heat melts aluminum directly onto the carbide tips.
Solutions for blade gumming:
A practical tip for how to cut thick aluminum without gumming: make multiple shallow passes rather than forcing through in one aggressive cut. This approach keeps heat manageable and allows chips to clear between passes.
Chipping—those ragged, torn edges that make your cuts look like something attacked them—typically plagues thin-wall profiles and hollow extrusions. The problem stems from vibration and insufficient material support during cutting.
Why chipping occurs:
Remedies for chip-free cuts:
When cutting aluminum with a jigsaw—a method some users attempt for curved cuts—chipping becomes especially problematic. The reciprocating blade action amplifies vibration in thin material. If jigsaw cutting is unavoidable, use fine-tooth metal blades (24+ TPI), apply cutting lubricant liberally, and keep feed rates very slow.
Nothing derails an extrusion project faster than cuts that aren't square. Even small deviations compound when you're assembling frames—gaps appear, joints don't align, and the entire structure suffers.
Common causes of out-of-square cuts:
How to cut extruded aluminum square every time:
The most common cutting mistake isn't using the wrong tool—it's ignoring feed rate. Too fast creates rough cuts and chipping. Too slow causes heat buildup and gumming. Finding the steady, moderate pace that produces continuous chips solves most quality problems.
Mastering these troubleshooting techniques transforms frustrating cutting sessions into predictable, professional results. But knowing how to solve problems is only half the equation—understanding which method to choose for your specific situation prevents problems from occurring in the first place. Let's bring everything together with a comprehensive comparison that matches each cutting method to its ideal applications.
You've explored each method in detail—now it's time to see them side by side. Choosing the best way to cut aluminium extrusion depends on your specific project requirements, budget, and skill level. This comprehensive comparison brings together everything we've covered, giving you a clear decision-making framework whether you're building your first aluminum frame or running production quantities.
Think of this section as your quick-reference guide. When you're standing in the shop wondering which tool to reach for, these tables and scenario recommendations will point you toward the right choice every time.
The following table compares all six cutting methods across the factors that matter most. We've positioned professional CNC services first as the precision benchmark, by DIY methods ranked by overall versatility and cut quality.
| Method | Tool Cost Range | Skill Level | Cut Quality | Best Use Cases | Key Limitations |
|---|---|---|---|---|---|
| Professional CNC Services | $1-3 per cut | None required | Excellent (±0.05mm) | High volume, tight tolerances, complex profiles | Lead time required, minimum orders may apply |
| Miter Saw | $150-400 + $40-80 blade | Beginner-friendly | Very Good (±1mm) | Frame building, T-slot extrusions, repeatable cuts | Limited stock length capacity |
| Circular Saw | $80-250 + $40-60 blade | Intermediate | Good (±2mm with guide) | Long stock, on-site cutting, sheet/plate work | Requires setup for straight cuts |
| Band Saw | $300-800+ | Intermediate | Excellent | Thin-wall tubing, hollow profiles, curved cuts | Slow cutting speed, larger footprint |
| Chop Saw (with proper blade) | $100-200 + $40-60 blade | Beginner | Fair to Good | Budget shops with existing equipment | Less precision, blade swap required |
| Hacksaw | $15-30 | Beginner | Fair | One-off cuts, small profiles, no-power situations | Extremely slow, physically demanding |
Notice how the relationship between cost and quality isn't linear. A saw for cutting aluminum at $200 with proper blade selection can outperform a $500 tool with wrong specifications. The blade—not the saw itself—determines most of your result quality when cutting aluminium with mitre saw or circular saw equipment.
Different projects demand different approaches. Use these scenario-based recommendations to match your specific situation with the optimal cutting method:
Building a 3D printer or CNC frame?
One-off repair or single bracket cut?
Production run of 100+ pieces?
Cutting thin-wall aluminum tubing?
On-site fabrication or job site work?
Working with complex multi-cavity extrusions?
Tight budget, occasional aluminum projects?
After analyzing all methods, here's how to cut aluminum extrusions based on your primary priority:
| Priority | Best Method | Why This Choice |
|---|---|---|
| Best for Beginners | Miter Saw | Fixed geometry removes variables; built-in precision features compensate for inexperience |
| Best for Precision | Professional CNC Services | ±0.05mm tolerances impossible with consumer equipment; perfect consistency across quantities |
| Best for Budget | Upgraded Chop Saw or Hacksaw | Uses existing equipment or minimal investment; acceptable results for non-critical work |
| Best for High Volume | Professional CNC Services | Time savings, zero blade wear, and consistency outweigh per-cut costs at scale |
| Best for Delicate Profiles | Band Saw | Gentle cutting action preserves thin walls; prevents deformation other methods cause |
| Best for Versatility | Circular Saw | Handles any stock length, portable, works on sheets and profiles equally |
Still uncertain which method fits your situation? Consider these decision points:
The truly best way to cut aluminum extrusion matches your method to your specific constraints. A hacksaw that gets the job done beats a miter saw you don't own. Professional services that deliver perfect cuts beat hours of frustration with inadequate equipment.
Whether you saw cut aluminum yourself or leverage professional processing, you now have the knowledge to achieve clean, precise results. The right tool exists for every scenario—from the hobbyist building their first frame to the manufacturer producing thousands of identical components. Choose based on your actual needs, not theoretical ideals, and your aluminum extrusion projects will come together exactly as designed.
For most users, a miter saw with a 60-80 tooth TCG (Triple Chip Grind) carbide-tipped blade delivers the best balance of precision, speed, and accessibility. The fixed fence and controlled blade entry produce consistently square cuts with minimal burr formation. For thin-wall or hollow profiles, band saws excel due to their gentle cutting action. Professional CNC cutting services remain the gold standard for high-volume orders or when tolerances below ±0.1mm are required.
Achieving clean cuts requires proper blade selection, correct speed settings, and adequate workpiece support. Use TCG geometry blades with 80+ teeth for smoother finishes. Apply wax stick lubricant to prevent aluminum gumming. Maintain steady, moderate feed pressure—too fast causes chipping while too slow generates heat that melts material onto blade teeth. Always clamp the extrusion securely and support the cut-off piece to prevent tearing at the blade exit point.
Yes, miter saws are the top-ranked method for cutting aluminum extrusion. The key is using the right blade—swap your wood blade for a carbide-tipped non-ferrous metal blade with TCG tooth geometry and 60-100 teeth. Avoid ATB blades designed for wood as they grab aluminum aggressively. Most 10-inch miter saws running at 3,800 RPM work well with aluminum when paired with proper blades and moderate feed rates.
The ideal blade features carbide-tipped teeth with TCG (Triple Chip Grind) geometry, a neutral or negative hook angle (0° to -5°), and 60-100 teeth depending on application. For general-purpose cutting, 80-tooth blades offer the best balance between speed and finish quality. Brands like Freud LU77M010 and Diablo consistently receive top recommendations. Reserve 100+ tooth blades for thin-wall profiles or visible joints requiring ultra-smooth edges.
Professional CNC cutting services make sense for high-volume orders (50+ pieces), ultra-tight tolerance requirements (±0.1mm or less), complex angle cuts, or when you lack proper equipment. Factory-direct suppliers like Shengxin Aluminium offer precise CNC machining with guaranteed squareness and burr-free edges. The per-cut cost often proves competitive when factoring in blade wear, setup time, and material waste from DIY learning curves.


 خدمة الإنترنت
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 العربية
 English
 français
 Deutsch
 русский
 español
 português
 ไทย
 Việt
 Українська