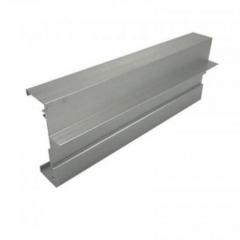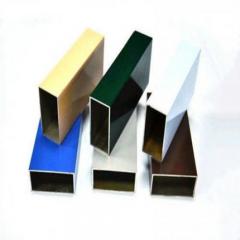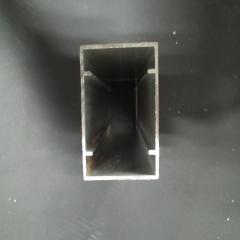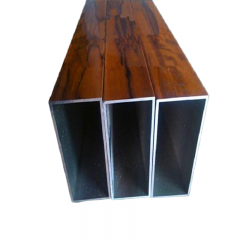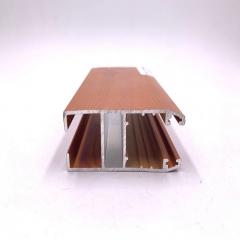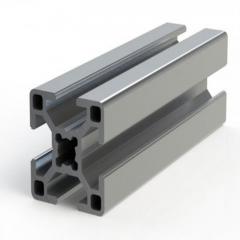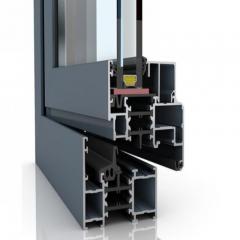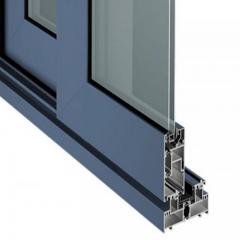
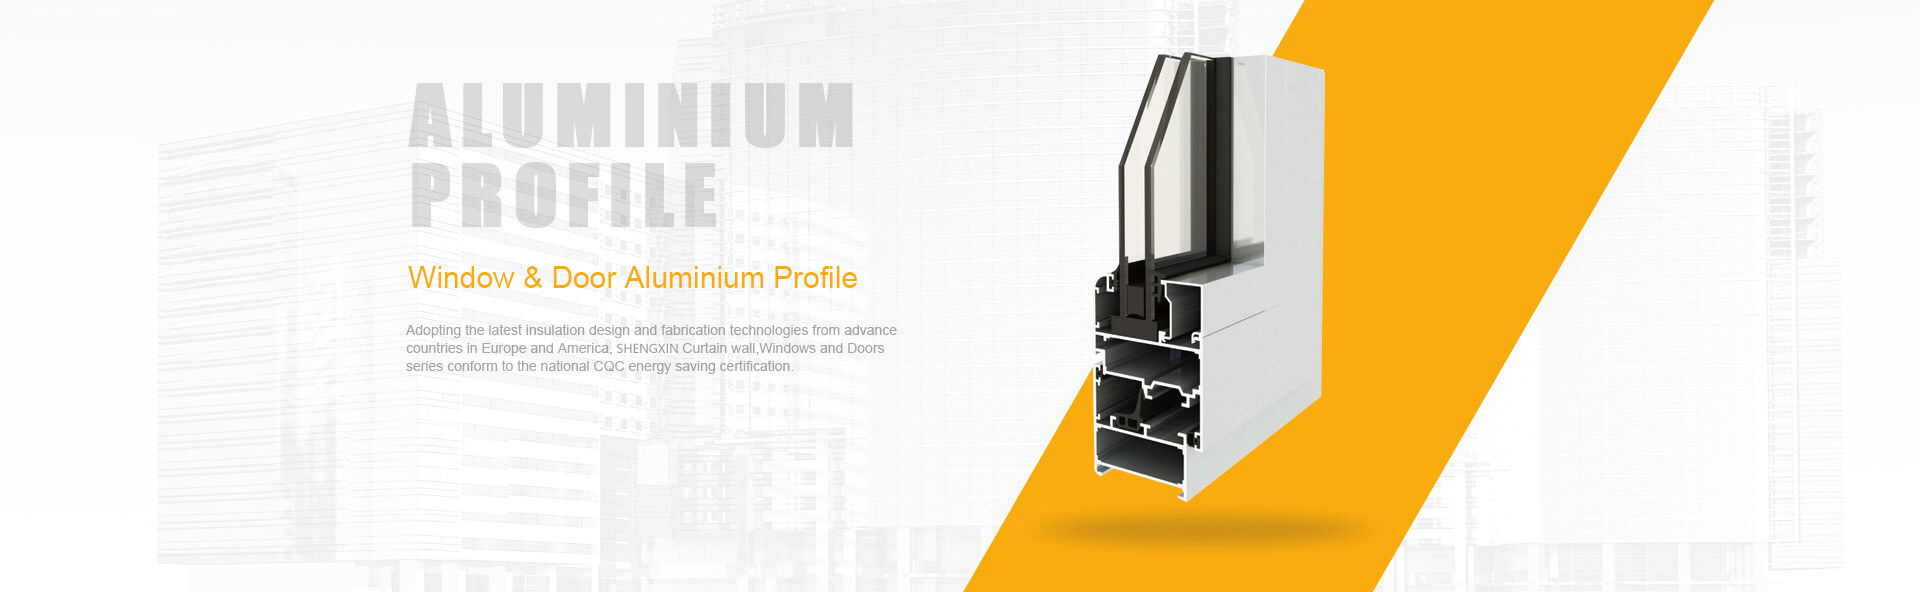
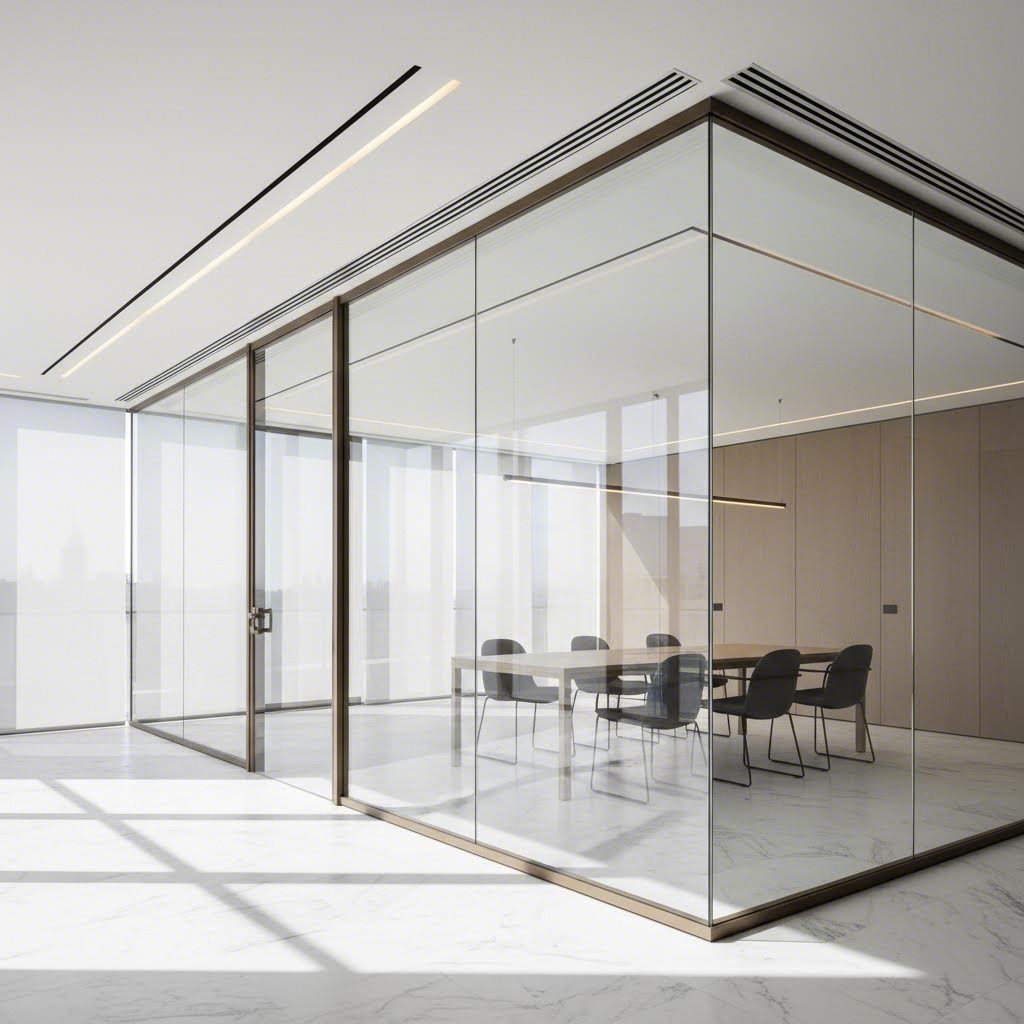
Imagine you're designing a sleek office partition or a stunning glass showcase for a retail store. How do you securely hold those glass panels in place while maintaining a clean, professional appearance? The answer lies in aluminum extrusion for glass panels—a manufacturing process that creates precisely engineered profiles to frame, support, and protect glass installations across countless applications.
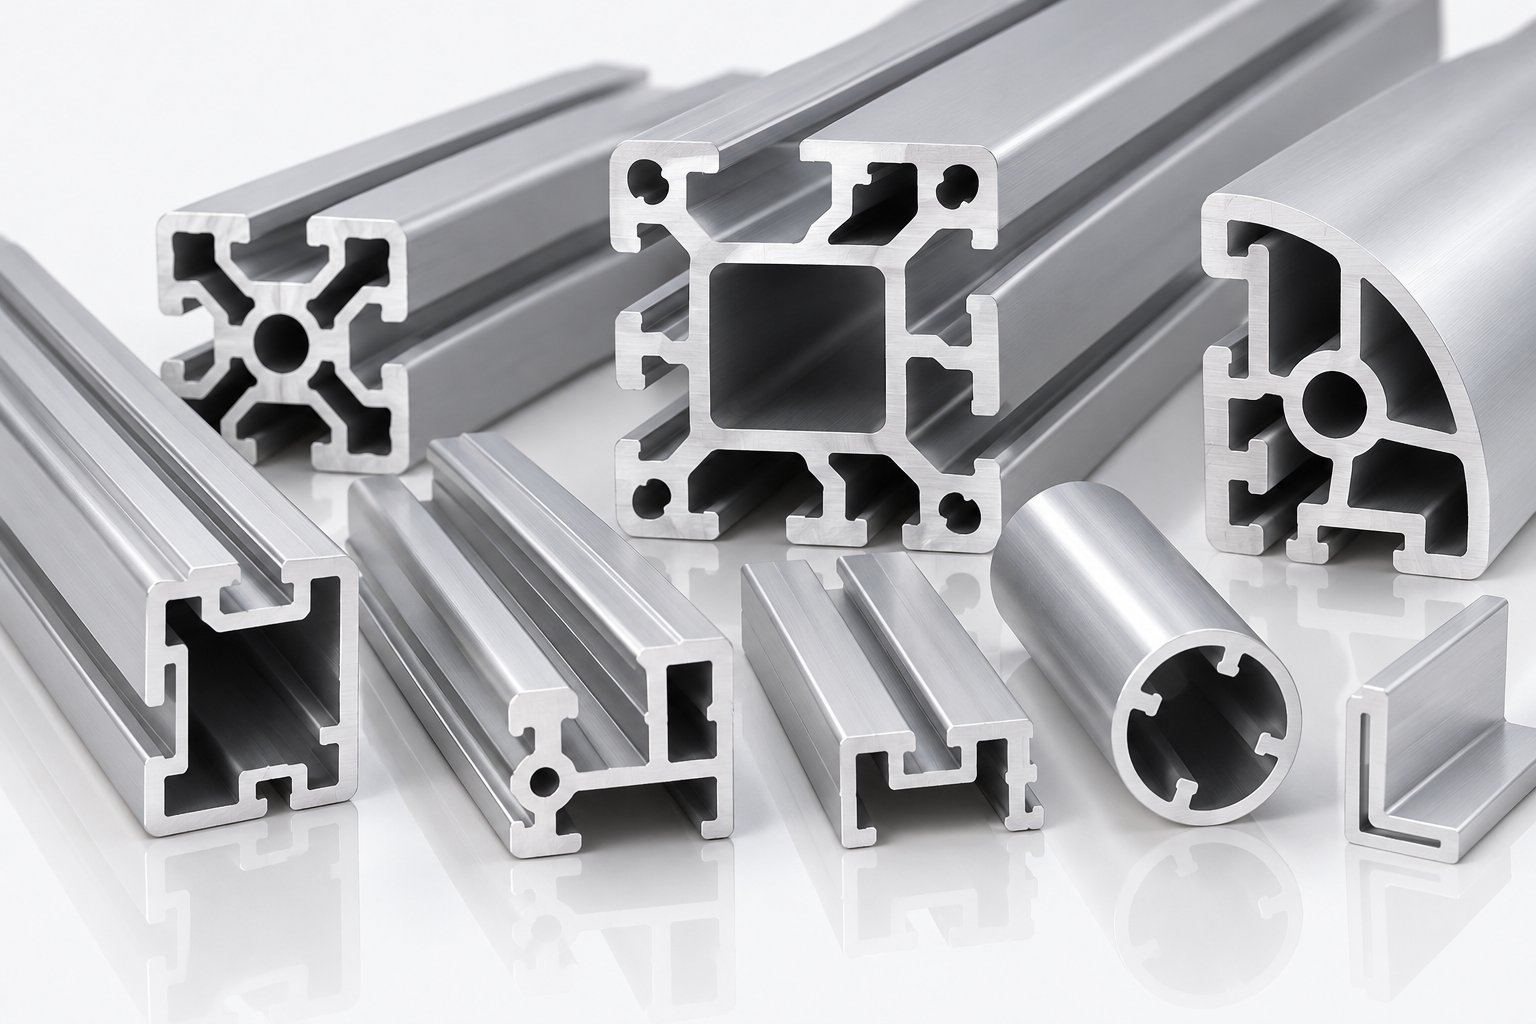
At its core, aluminum extrusion is a process where heated aluminum alloy is pushed through a specially designed die to create specific cross-sectional shapes. Think of it like squeezing toothpaste through a tube, except the opening is engineered to produce exact profiles that perfectly accommodate glass panels. These profiles can be solid, hollow, or semi-hollow, ranging from simple channels to complex multi-chamber designs with integrated features.
The fundamental purpose of this technology is straightforward: creating secure, aesthetically pleasing connections between glass panels and structural elements. Whether you're working on architectural glazing, interior partitions, or display cases, aluminum extrusions for panels provide the framework that makes modern glass installations possible.
Why has this become the industry standard? The answer involves several key advantages that aluminum brings to glass applications:
Every extrusion frame starts with a custom-designed die—a steel disc with a precisely cut opening that determines the profile's final shape. When heated aluminum billet is forced through this die under tremendous pressure, it emerges as a continuous length of material with the exact cross-section needed for your glass panel application.
After extrusion, profiles typically undergo heat treatment to enhance their mechanical properties. According to Gabrian International, heat-treated 6061 aluminum achieves a tensile strength of 310 MPa compared to 241 MPa in its untreated state—a significant improvement for structural applications.
The versatility of aluminum panel extrusions explains their dominance in glass applications. From a simple aluminum extrusion case for museum displays to elaborate curtain wall systems on commercial buildings, the same fundamental process creates solutions for every scale. Profiles can be fabricated with punched holes, machined grooves, and cut to exact lengths, allowing seamless integration with hardware and other building systems.
What makes this technology particularly valuable for glass showcase applications is its design flexibility. Unlike welded or cast alternatives, extruded aluminum allows for complex geometries—including channels for drainage, pockets for gaskets, and integrated mounting features—all formed in a single manufacturing step. This precision ensures consistent quality across every piece while keeping costs manageable for both standard and custom projects.
Now that you understand how aluminum extrusions are formed, the next critical question emerges: which aluminum alloy should you specify for your glass panel project? This decision directly impacts everything from structural performance to final appearance—yet many sources mention alloy options without explaining the meaningful differences between them.
When reviewing aluminum profile extrusions for glass applications, you'll frequently encounter two alloy designations: 6063 and 6005A. Both belong to the 6000 series aluminum family (alloyed with magnesium and silicon), but their performance characteristics differ significantly. Understanding these distinctions helps you match the right material to your specific project requirements.
If you examine most aluminum extrusions used in visible glass applications—storefront systems, interior partitions, display cases—you'll find 6063-T5 or 6063-T6 aluminum. Why has this alloy become the industry favorite?
The answer lies in its exceptional combination of properties. According to material selection guidelines from Yaji Aluminum, 6063-T5 offers an excellent balance of strength, corrosion resistance, formability, and aesthetic surface finish. Its high extrudability allows manufacturers to create intricate profile shapes with thin walls and sharp details—essential when you need precise channels for glass panels and gaskets.
What makes 6063 particularly valuable for aluminium extrusions in architectural settings is its superior surface quality. The alloy's fine grain structure produces smooth, uniform surfaces that respond beautifully to anodizing and powder coating. When your glass framing will be visible to building occupants or customers, this aesthetic quality matters tremendously.
So when would you choose 6005A over the more common 6063? The answer centers on structural demands. While 6063 handles most architectural glazing applications admirably, 6005A provides approximately 20-30% higher tensile and yield strength. This makes it the preferred choice when your extruded aluminum sections must bear significant loads or span greater distances without intermediate support.
Consider applications like large commercial curtain walls, glass railings with minimal visible framing, or canopy systems where the aluminum extrusion bar must resist substantial wind loads. In these scenarios, 6005A's enhanced mechanical properties justify its slightly reduced extrudability and surface finish quality.
The trade-off is straightforward: 6005A achieves higher strength but produces a marginally coarser surface texture that may show more visible grain after anodizing. For hidden structural members or applications where strength trumps appearance, this compromise makes perfect sense.
| Property | 6063-T5/T6 | 6005A-T5/T6 |
|---|---|---|
| Tensile Strength | ≥157 MPa (T5) / ≥205 MPa (T6) | ≥255 MPa (T5/T6) |
| Yield Strength | ≥108 MPa (T5) / ≥170 MPa (T6) | ≥215 MPa (T5/T6) |
| Extrudability Rating | Excellent—complex thin-wall profiles possible | Good—some limitations on intricate details |
| Corrosion Resistance | Excellent—ideal for exterior exposure | Very Good—performs well in most environments |
| Surface Finish Quality | Superior—smooth, uniform appearance | Good—slightly coarser grain visible |
| Typical Applications | Storefronts, interior partitions, display cases, residential windows | Structural glazing, large-span curtain walls, load-bearing frames |
How do you decide between these alloys? Start by evaluating your project's primary requirements:
For most glass panel applications—particularly interior partitions, showcases, and standard window framing—6063-T5 remains the optimal choice. Its proven performance, widespread availability, and aesthetic versatility make it the default specification for architects and fabricators alike. Reserve 6005A for those projects where structural calculations demand its enhanced strength, and you'll achieve the ideal balance of performance and appearance for your specific glass installation needs.
You've selected the right aluminum alloy for your project—but how do you ensure the extrusion profile actually fits your glass? This seemingly simple question trips up many first-time specifiers. The truth is, aluminum window extrusions aren't one-size-fits-all solutions. Every profile is engineered to accommodate specific glass dimensions, and choosing the wrong channel depth can lead to installation failures, glass stress fractures, or compromised weatherproofing.
Understanding how glass thickness relates to profile design is essential whether you're ordering standard catalog profiles or developing custom aluminium window extrusions for a specialty application.
When you examine a typical window extrusion cross-section, you'll notice a channel or groove designed to receive the glass panel. This channel isn't simply the same width as the glass—it must account for several additional factors that ensure proper installation and long-term performance.
The channel depth refers to how far the glass sits into the aluminum profile. Too shallow, and the glass lacks adequate support; too deep, and you may struggle to install gaskets or achieve proper sight lines. Most aluminum window extrusion profiles follow established industry guidelines that match common glass thicknesses:
| Glass Thickness | Nominal Dimension | Recommended Channel Depth | Typical Applications |
|---|---|---|---|
| 1/8 inch | 3 mm | 10-12 mm | Picture frames, light display cases |
| 3/16 inch | 5 mm | 12-15 mm | Cabinet doors, interior partitions |
| 1/4 inch | 6 mm | 15-18 mm | Standard windows, shower enclosures |
| 3/8 inch | 10 mm | 20-25 mm | Commercial storefronts, safety glazing |
| 1/2 inch | 12 mm | 25-30 mm | Heavy-duty applications, insulated units |
Notice how the channel depth exceeds the glass thickness in every case? That extra space serves critical functions—accommodating gaskets, allowing for thermal movement, and providing adequate bite depth for structural security.
Beyond simple thickness matching, several compatibility considerations determine whether a particular aluminium extrusion rail will work for your glass application. According to ISOGOM's installation guidelines, proper measurement ensures a uniform seal and prevents gaps—critical for both weatherproofing and long-term durability.
Here are the key factors you'll need to evaluate:
What happens when standard profiles don't match your requirements? This is where custom aluminum extrusion panels come into play. For non-standard glass thicknesses or specialty applications, manufacturers can develop project-specific profiles with precisely engineered channel dimensions.
Laminated glass, for example, requires deeper channels than monolithic glass of equivalent total thickness because the interlayer adds manufacturing tolerance variations. A 1/4 inch laminated panel (two 3 mm lites with a PVB interlayer) may actually measure anywhere from 6.4 mm to 6.8 mm—your profile must accommodate the maximum dimension while still providing adequate gasket compression at the minimum.
Insulated glass units present even greater challenges. A typical residential IGU with two 3 mm lites and a 12 mm air space creates a total assembly thickness around 18-20 mm—requiring substantially different profile geometry than single-glazed applications. These units also weigh considerably more, demanding reinforced aluminum sections with greater wall thickness and structural depth.
When specifying profiles for specialty glass, always verify the actual measured thickness of your glass product rather than relying solely on nominal dimensions. Manufacturing tolerances vary between suppliers, and even small discrepancies can create installation problems or compromise seal effectiveness. With the right profile matched to your specific glass dimensions, you'll achieve secure installations that perform reliably for decades.
So you've matched your glass thickness to the right profile channel—but here's where many projects go sideways. Are you framing a stationary interior partition or a functioning glass door? The answer dramatically changes your aluminum frame extrusions requirements, and treating these applications identically is a recipe for premature failure.
Think about it: a fixed glass wall simply stands in place, supporting its own weight while occasionally resisting someone leaning against it. A glass door, however, swings open hundreds of times daily, absorbs the shock of enthusiastic closures, and must securely anchor heavy hardware that transfers significant forces into the frame. These fundamentally different stress patterns demand equally different extrusion specifications.
Interior glass walls have become architectural staples in modern offices, conference rooms, and retail environments. They create visual openness while providing acoustic separation—and their aluminum door frame extrusions reflect these priorities.
For stationary partitions, your profile selection typically emphasizes three factors:
Typical interior partition profiles weigh between 0.3 and 0.8 kg per linear meter—relatively lightweight because they don't need to resist operational stresses. The extruded aluminum door frame for a fixed partition can use thinner wall sections (1.2-1.6 mm) since loads remain static and predictable.
Where does an aluminum extrusion slider fit into partition systems? Many modern office layouts incorporate sliding glass panels that stack or pocket into walls. These applications bridge the gap between fixed partitions and swinging doors, requiring track systems and aluminum window frame extrusions that support smooth horizontal movement while maintaining acoustic performance.
Now consider what happens when that glass panel becomes a functioning door. Every component must handle dynamic forces that fixed partitions never experience:
These demands explain why aluminum door frame extrusions typically weigh 1.0 to 2.5 kg per linear meter—sometimes three times heavier than partition profiles. Wall thicknesses increase to 2.0-3.0 mm, and profile designs incorporate reinforcement features specifically for hardware integration.
Hardware compatibility represents one of the most overlooked specification details. When you select an extruded aluminum slide track for a bypass door system or hinge pockets for a swing door, consider these integration requirements:
| Specification | Interior Partition Profiles | Glass Door Profiles |
|---|---|---|
| Typical Profile Weight | 0.3-0.8 kg/m | 1.0-2.5 kg/m |
| Wall Thickness | 1.2-1.6 mm | 2.0-3.0 mm |
| Hardware Integration | Minimal—basic floor guides and head channels | Extensive—hinge pockets, lock blocks, closer reinforcement |
| Recommended Alloy | 6063-T5 (aesthetics prioritized) | 6063-T6 or 6005A-T6 (strength prioritized) |
| Key Performance Requirements | Visual minimalism, acoustic sealing, easy installation | Fatigue resistance, hardware anchorage, impact durability |
| Typical Cycle Rating | N/A (static application) | 100,000-500,000 open/close cycles |
Notice the alloy recommendations differ between applications. While 6063-T5 works beautifully for fixed partitions where appearance matters most, door frames often benefit from the T6 temper or 6005A alloy to handle repeated stress cycles without developing fatigue cracks at hardware attachment points.
What about glass doors in high-traffic commercial environments? These applications push specifications even further. Automatic sliding entrance systems, for instance, combine the horizontal movement of an extruded aluminum slide with motorized operators that impose additional forces on track and header profiles. Panic hardware on emergency exits must remain functional after years of dormancy, then perform flawlessly during an evacuation—demanding profiles specifically engineered for these critical life-safety applications.
The key takeaway? Never assume a profile designed for stationary glass walls will perform adequately as a door frame. By specifying the appropriate extrusion weight class, wall thickness, and hardware integration features from the start, you'll avoid the costly callbacks and premature failures that plague under-specified glass door installations.
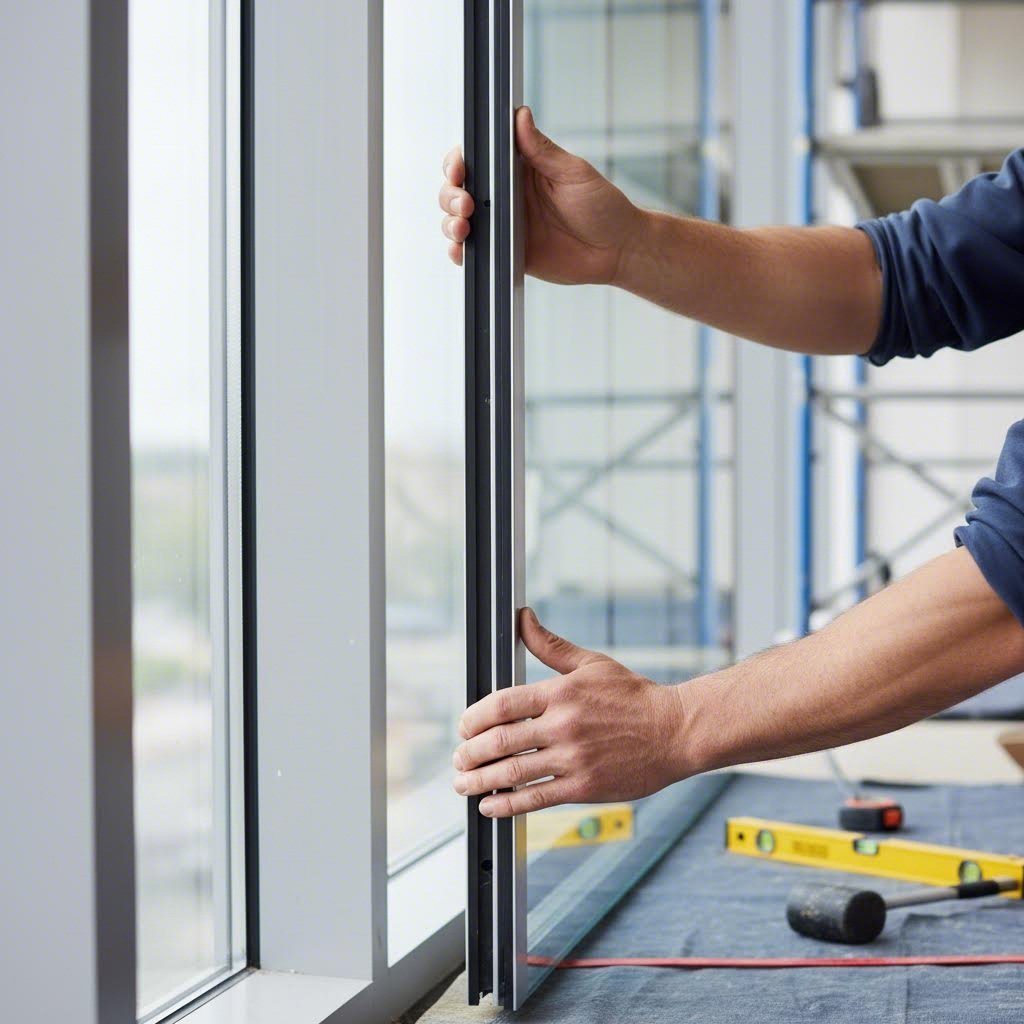
You've selected the right alloy, matched your profile to the glass thickness, and chosen appropriate extrusions for your application type. Now comes the moment of truth: actually installing everything. This is where many projects stumble—not because the components are wrong, but because installation technique makes the difference between a flawless glass wall and one that leaks, rattles, or develops stress cracks within months.
Whether you're a DIY fabricator tackling your first aluminum extrusion assembly or a seasoned professional refining your approach, the principles remain consistent. Proper installation protects your glass investment, ensures long-term performance, and delivers the clean sight lines that make aluminum-framed glass installations so visually appealing.
Before touching any glass, your aluminum framing must be completely assembled, leveled, and secured. Rushing this preparation phase virtually guarantees problems during glazing. Here's the sequential process that professionals follow:
Beyond the basic sequence, several techniques separate amateur installations from professional-quality results. Understanding these nuances helps you achieve installations that perform reliably for decades.
These two fundamental approaches to securing glass within aluminium track extrusions offer different advantages:
Many commercial systems combine both methods—using dry gaskets for primary glass retention while adding sealant beads at critical weatherproofing locations.
Glass fails when subjected to concentrated stress, and improper installation creates exactly those conditions. Follow these practices to protect your glazing:
For exterior applications, water infiltration represents the primary performance concern. Your aluminum extrusion assembly must address multiple water management strategies:
The visual appeal of glass installations depends largely on consistent, crisp frame lines. Achieve professional results by:
The difference between acceptable and exceptional glass installations often comes down to the final fifteen minutes—taking time to verify alignment, clean surfaces, and correct minor imperfections before walking away.
Whether you're installing a simple display case or a complex curtain wall system, these fundamental techniques scale appropriately. DIY fabricators working with an aluminum extrusion kit can achieve professional results by following these principles carefully, while commercial installers use the same methods at higher speed across larger projects. The key is never compromising on preparation, sequencing, or attention to the details that determine long-term performance.
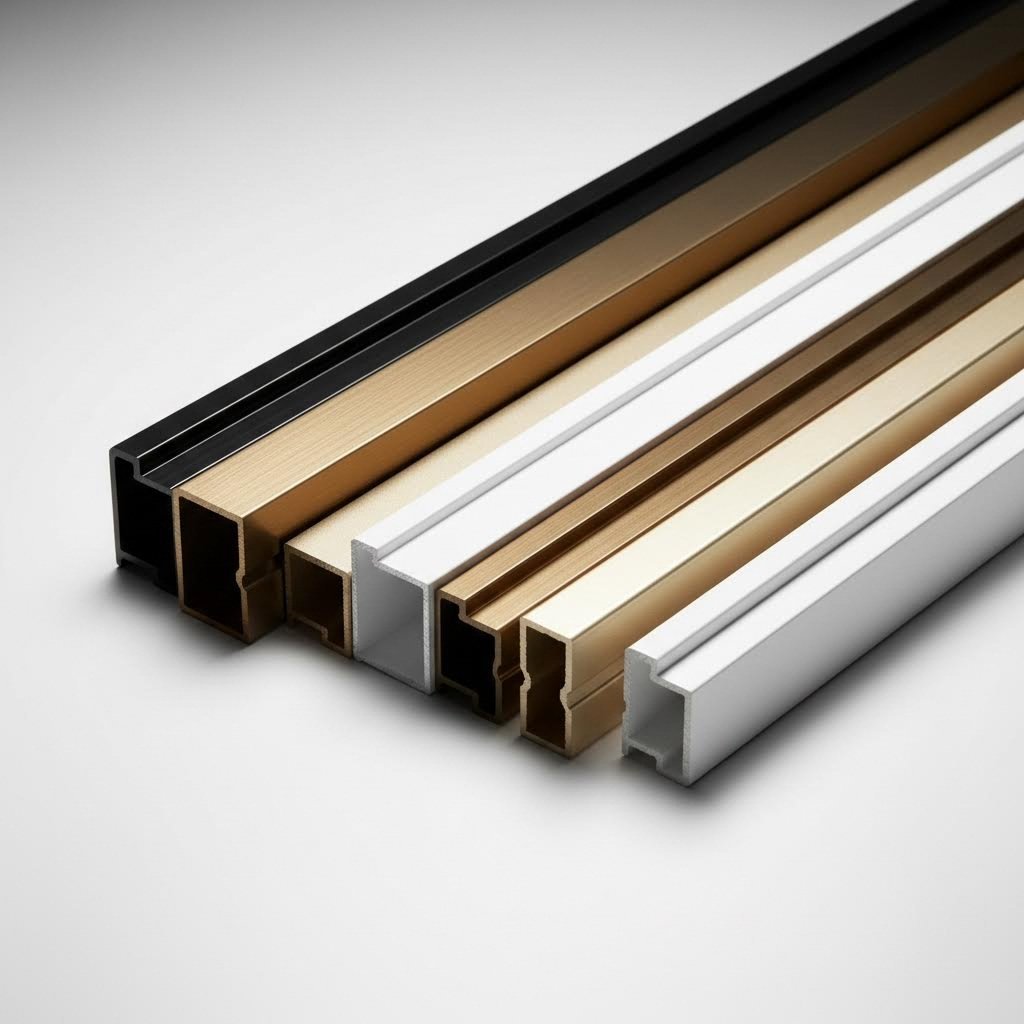
Your aluminum profiles are installed, your glass is set—but what about that raw aluminum surface? Left untreated, even the finest 6063 alloy will eventually oxidize unevenly, collect dirt, and detract from your glass installation's appearance. Surface treatments transform functional aluminum extrusion trim into architectural elements that complement your glazing for decades.
The finish you choose affects far more than aesthetics. Corrosion resistance, UV stability, color matching capabilities, and long-term maintenance requirements all depend on selecting the right treatment for your specific application. Let's explore your options from basic to advanced.
Anodizing remains the most popular finish for architectural glazing applications—and for good reason. This electrochemical process converts the aluminum surface into a hard, integral oxide layer that becomes part of the metal itself rather than sitting on top like paint.
What makes anodizing particularly valuable for glass panel framing? The resulting surface is exceptionally hard (harder than steel in some cases), scratch-resistant, and permanently bonded to the substrate. Unlike coatings that can chip or peel, anodized aluminium extrusion trim maintains its appearance even after years of contact with cleaning equipment and daily use.
Your anodizing options include:
For extruded aluminum enclosures and display cases where fingerprints and frequent handling are concerns, anodized finishes offer easy maintenance—a simple wipe removes most marks without damaging the surface.
When your design calls for specific colors that anodizing cannot achieve—or when budget constraints favor applied coatings—powder coating and PVDF (polyvinylidene fluoride) finishes enter the conversation.
Powder coating applies dry powder electrostatically, then cures it under heat to form a durable polymer film. This process offers virtually unlimited color matching, including custom RAL colors, metallics, and textured finishes. For interior applications and protected exterior locations, quality powder coating provides excellent durability at moderate cost.
However, standard powder coatings can fade or chalk when exposed to intense UV radiation over extended periods. This limitation matters significantly for south-facing curtain walls or storefronts in sunny climates.
PVDF coating (often marketed under brand names like Kynar) addresses this UV vulnerability. These fluoropolymer finishes maintain color stability for 20-30 years even under harsh sun exposure. Major architectural projects typically specify PVDF for exterior aluminum framing precisely because of this proven longevity.
| Finish Type | Corrosion Resistance | UV Stability | Color Options | Best Applications |
|---|---|---|---|---|
| Mill Finish | Moderate | Poor—oxidizes unevenly | Natural aluminum only | Concealed framing, temporary installations |
| Clear Anodize | Excellent | Excellent | Natural metallic | Contemporary interiors, protected exteriors |
| Color Anodize | Excellent | Very Good | Limited palette (bronze, black, gold tones) | Architectural glazing, display cases |
| Powder Coating | Very Good | Good (interior) / Moderate (exterior) | Unlimited—any RAL color | Interior partitions, protected locations |
| PVDF Coating | Excellent | Exceptional—20+ year stability | Wide palette with metallics | Exterior curtain walls, storefronts |
| Micro-arc Oxidation | Superior | Excellent | Limited (ceramic-like appearance) | High-wear applications, specialty projects |
For those designing an aluminium extrusion box or extruded aluminum housing for electronics or display purposes, the finish selection also impacts thermal properties. Dark anodized or powder-coated surfaces absorb more heat than white aluminum profile finishes—a consideration when internal components are heat-sensitive.
Specialty finishes like micro-arc oxidation (also called plasma electrolytic oxidation) create ceramic-like surfaces with exceptional hardness and wear resistance. While more expensive than conventional treatments, these finishes serve demanding applications where standard options fall short.
How do you match your aluminum framing to adjacent glass? Consider that glass reflects its surroundings while aluminum absorbs or reflects light depending on finish. Dark bronze anodized frames visually recede, emphasizing glass transparency. White aluminum profile finishes create crisp contrast against tinted glass. Metallic PVDF coatings can echo reflective glass surfaces for unified facades.
Interior versus exterior placement significantly influences your decision. Interior applications prioritize aesthetics and touchability—anodized finishes excel here. Exterior installations demand weathering performance first, making PVDF the professional's choice for exposed glazing systems. Manufacturers like Shengxin Aluminium offer comprehensive surface treatment options including anodizing in custom colors, powder coating, PVDF, and micro-arc oxidation—allowing you to specify exactly the right finish for your project's requirements.
With the right surface treatment selected, your aluminum extrusions will complement your glass panels beautifully while resisting the environmental challenges of their intended location. But what about specialized applications like retail showcases or cabinet systems? These present unique requirements that standard architectural specifications may not address.
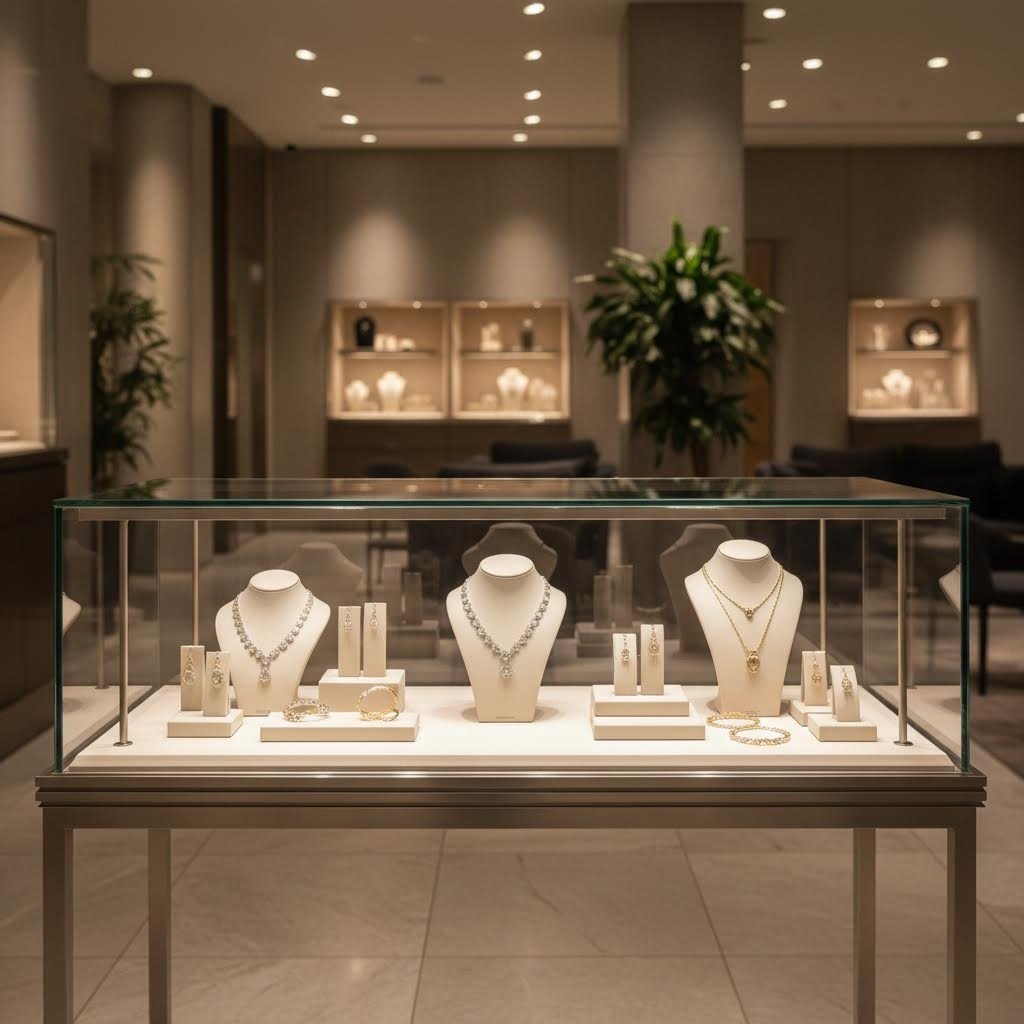
Beyond architectural glazing and interior partitions, aluminum extrusions paired with glass panels serve countless specialized applications where precision, security, and aesthetics intersect. Walk into any jewelry store, museum gallery, or modern kitchen, and you'll encounter glass show case systems and cabinet installations that rely on purpose-designed aluminum profiles to protect, display, and organize valuable contents.
These specialized applications demand more than standard window framing can deliver. An aluminum extrusion display case for a luxury watch retailer must deter theft while maximizing product visibility. Museum showcases require climate control integration and UV filtering. Kitchen cabinet doors need smooth operation over thousands of cycles. Each scenario calls for extrusion profiles engineered to specific performance criteria.
Ever notice how high-end retail displays seem to float merchandise in space? That visual magic comes from carefully engineered aluminum profiles that minimize visible framing while providing robust security. Retail glass show case systems balance several competing demands:
Security considerations drive significant design differences. Retail aluminum extrusion cabinet systems often incorporate locking mechanisms concealed within the profile, reinforced corners resistant to prying, and laminated glass retention features that prevent smash-and-grab theft. The extrusion cross-section may include internal channels specifically sized for steel reinforcement bars or electronic sensor wiring.
Museum applications prioritize environmental control over theft prevention. Here, aluminum extrusion cabinets feature sealed gasket systems that maintain stable humidity levels, integrated channels for fiber-optic or LED lighting that won't emit damaging heat, and provisions for silica gel or other desiccant materials. The precision tolerances required—often ±0.1mm—exceed typical architectural specifications.
Lighting integration deserves special attention. Many aluminum extrusion furniture applications and display cases incorporate dedicated channels for LED strip lighting. These channels position lights to illuminate contents without creating glare on glass surfaces—a technical challenge that requires careful geometric planning during the extrusion die design phase.
Cabinet applications bring aluminum and glass together in contexts ranging from kitchen renovations to office storage systems. Unlike fixed display cases, cabinet doors must operate smoothly while maintaining alignment over years of daily use.
The aluminum cabinet door extrusion market serves diverse needs:
What distinguishes cabinet door profiles from showcase framing? Weight optimization becomes critical when doors must swing or slide repeatedly. Aluminum extrusion furniture components typically use thinner wall sections—sometimes as light as 1.0mm—while maintaining adequate stiffness through clever profile geometry. The cross-section might incorporate internal ribs or hollow chambers that add rigidity without adding mass.
Hardware integration also differs substantially. Cabinet door extrusions must accommodate concealed hinges, soft-close mechanisms, and handle mounting—all while maintaining clean exterior lines. Many profiles include pre-formed channels that accept standard European cabinet hardware without additional machining.
How does application priority influence design? Consider these distinctions:
For DIY builders and custom fabricators, the plexiglass aluminum frame combination offers particular advantages. Acrylic panels weigh significantly less than glass, reducing hardware demands while eliminating breakage concerns. Many standard extrusion profiles accept either material, giving designers flexibility based on specific project requirements.
Whether you're specifying showcases for a new retail concept or selecting cabinet door framing for a kitchen renovation, understanding how extrusion design serves different priorities helps you choose profiles that perform precisely as intended. The next consideration—sourcing these specialized profiles—determines whether your vision becomes reality through standard catalog options or custom extrusion development.
You've identified exactly which profile geometry, alloy specification, and surface treatment your glass panel application requires. Now comes the practical question that determines project success: where do you actually source these components? The answer isn't as simple as browsing an aluminum extrusions for sale listing—your sourcing strategy directly impacts quality, lead time, cost, and ultimately whether your finished installation meets expectations.
Whether you're a DIY fabricator building a single display case or a professional specifier managing commercial glazing projects, understanding the landscape of aluminum extrusion supply helps you make informed decisions. Let's navigate the path from initial specification through supplier selection to final delivery.
Your first major decision involves choosing between standard catalog profiles and custom extrusion development. This isn't simply a cost calculation—it's a strategic choice that affects design flexibility, project timeline, and long-term value.
Standard profiles from established suppliers like CR Laurence aluminum catalogs or CRL U.S. aluminum distributors offer immediate advantages. These pre-engineered shapes have been refined through thousands of installations, incorporating lessons learned about gasket compatibility, hardware integration, and structural performance. When a standard profile matches your requirements, you benefit from proven designs without development costs or delays.
Where do you find these options? An extruded aluminum shapes catalog from major glazing suppliers typically includes:
However, standard profiles impose design constraints. You're limited to available dimensions, and your project must adapt to existing geometries rather than the reverse. When off-the-shelf options don't quite fit—perhaps you need a specific channel depth for laminated glass, integrated hardware mounting features, or unique aesthetic details—custom extrusion development becomes the path forward.
Custom die development involves engineering a new extrusion die specifically for your project. The manufacturer creates precision tooling that produces profiles matching your exact specifications. According to industry guidelines, die costs typically range from $500 to $5,000 depending on profile complexity, with tooling lead times of 2-4 weeks before production begins.
| Factor | Standard Catalog Profiles | Custom Extrusions |
|---|---|---|
| Initial Cost | Lower—no die development charges | Higher—tooling investment of $500-$5,000+ |
| Availability | Immediate—typically ships within days | Extended—2-4 weeks tooling plus production time |
| Design Options | Limited to existing aluminum shapes catalog | Unlimited—any feasible cross-section |
| Project Optimization | May require design compromises | Profile engineered to exact requirements |
| Minimum Order | Often available in small quantities | Typically requires larger runs to justify tooling |
| Future Reorders | Always available from stock | Die retained for repeat orders at production cost only |
| Best For | Standard applications, small projects, tight timelines | Unique requirements, large volumes, recurring needs |
How do you decide which approach suits your project? Consider these questions:
For many architectural applications, the answer involves both approaches. You might select standard profiles for straightforward framing while developing custom extrusions for specialized components like corner assemblies or hardware mounting sections.
Once you've determined your sourcing approach, selecting the right manufacturer becomes critical. Not all aluminum extrusion suppliers offer equivalent capabilities, and mismatched expectations create project delays, quality issues, and budget overruns.
What separates reliable partners from problematic suppliers? Industry experts emphasize several evaluation criteria that predict supplier performance:
Extrusion presses are rated by tonnage, and this specification determines what profiles a manufacturer can produce. Small presses (under 1,000 tons) handle lightweight profiles efficiently but cannot produce large structural sections. Massive presses (3,000-5,500 tons) create heavy industrial profiles but may be inefficient for delicate architectural trim.
Look for manufacturers with diverse press capacity ranges. Shengxin Aluminium, for example, operates 35 extrusion presses ranging from 600T to 5500T—providing flexibility to match the right equipment to each project's requirements. This breadth means your supplier can handle everything from fine-detailed item extruded aluminium trim to heavy structural framing without subcontracting.
Raw extrusions rarely install directly. Most applications require secondary operations: cutting to length, drilling mounting holes, machining notches for hardware, or creating complex joinery. Suppliers with integrated CNC machining centers deliver finished components ready for assembly rather than raw profiles requiring additional fabrication.
Ask potential suppliers about their machining capabilities:
Your previous finish selection means nothing if your supplier cannot deliver it. Verify that potential partners offer your required surface treatments in-house or through established finishing partners. In-house finishing typically provides better quality control and faster turnaround than outsourced processing.
Comprehensive suppliers offer multiple treatment options—anodizing in standard and custom colors, powder coating with extensive RAL color matching, PVDF for exterior durability, and specialty finishes like micro-arc oxidation. This breadth allows you to specify exactly the right finish without supplier limitations constraining your design.
The best suppliers function as partners rather than order-takers. They provide engineering support during design development, help optimize profiles for manufacturability, and troubleshoot issues before they become problems.
When evaluating technical support, consider:
Manufacturers with deep experience—like those with 30+ years in the industry—bring institutional knowledge that prevents common mistakes and identifies optimization opportunities less experienced suppliers might miss.
How do you verify that a supplier actually delivers claimed quality? Certifications provide third-party validation of manufacturing capabilities and quality management systems.
ISO 9001 certification indicates the supplier follows documented quality procedures with consistent inspection and traceability. According to manufacturing experts, this certification ensures consistent dimensions and properties, reliable surface finish quality, documentation of lot history for traceability, and clear processes for addressing any defects.
Request sample profiles before committing to large orders. Examine dimensional accuracy, surface finish quality, and overall workmanship. Reputable suppliers welcome this scrutiny—they know their products will impress.
Clear communication prevents disputes. Before ordering, establish explicit quality requirements including:
The most successful projects result from partnerships where both parties understand expectations before production begins—not disputes after delivery.
For projects requiring end-to-end support from die development through mass production, integrated manufacturers streamline the entire process. Shengxin Aluminium's deep processing services exemplify this comprehensive approach—combining extensive press capacity, CNC machining centers, multiple surface treatment options, and technical support under one roof. This integration eliminates coordination between multiple vendors while ensuring consistent quality throughout production.
Whether you're sourcing standard profiles from established distributors or developing custom extrusions with specialized manufacturers, thorough supplier evaluation protects your project investment. Take time to verify capabilities, request samples, review certifications, and establish clear quality expectations. The effort invested in selecting the right partner pays dividends through successful installations that perform reliably for years to come.
6063 aluminum offers excellent extrudability, superior surface finish quality, and corrosion resistance, making it ideal for visible architectural glazing like storefronts and display cases. 6005A provides 20-30% higher tensile and yield strength, best suited for structural applications like large curtain walls or glass railings where load-bearing capacity is critical. Choose 6063-T5/T6 when aesthetics matter most; select 6005A-T6 when structural demands require enhanced strength.
Extrusion channel depth must exceed glass thickness to accommodate gaskets, thermal expansion, and setting blocks. For 1/4 inch (6mm) glass, use 15-18mm channel depth; for 1/2 inch (12mm) glass, specify 25-30mm channels. Always allow 3-6mm edge clearance for thermal movement, ensure 15-25% gasket compression, and use setting blocks at quarter points along the bottom edge to properly support and center the glass.
Anodizing provides exceptional hardness, scratch resistance, and is permanently bonded to the aluminum—ideal for high-touch applications like display cases. Powder coating offers unlimited color matching for interior applications. PVDF coatings deliver 20-30 year UV stability for exterior curtain walls and storefronts. Clear anodize preserves natural metallic appearance, while color anodize adds bronze, black, or champagne tones for architectural aesthetics.
Standard profiles from suppliers like CRL offer immediate availability, proven designs, and lower costs—ideal for standard applications and tight timelines. Custom extrusions require tooling investment ($500-$5,000) and 2-4 week lead times but provide exact specifications for unique requirements. Choose custom when standard options meet less than 90% of requirements, project volumes justify tooling costs, or specific hardware integration features are needed.
Interior partition profiles weigh 0.3-0.8 kg/m with 1.2-1.6mm wall thickness, prioritizing aesthetic minimalism and acoustic sealing. Glass door profiles weigh 1.0-2.5 kg/m with 2.0-3.0mm walls, designed for hinge loads, impact forces, and hardware mounting. Door frames require reinforcement channels, mounting boss locations, and fatigue resistance rated for 100,000-500,000 open/close cycles that static partitions don't need.


 خدمة الإنترنت
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 العربية
 English
 français
 Deutsch
 русский
 español
 português
 ไทย
 Việt
 Українська