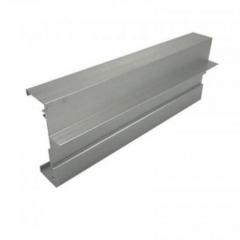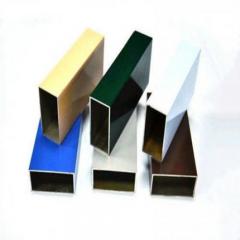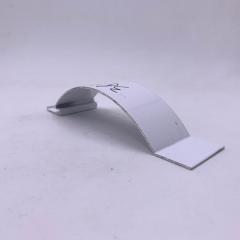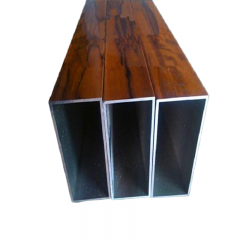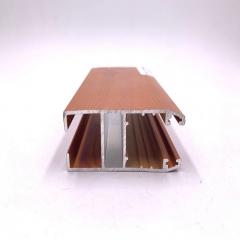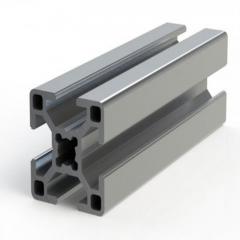
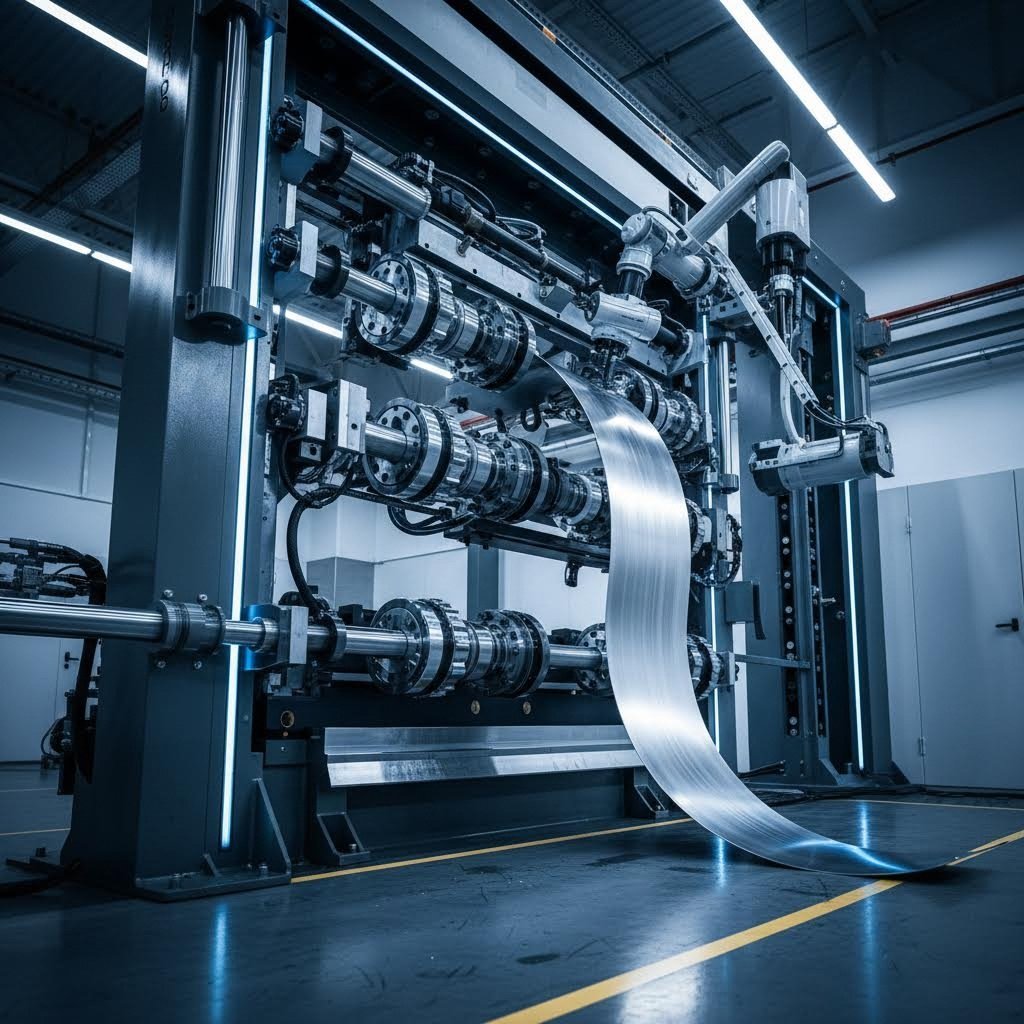
Imagine transforming a straight aluminum profile into a graceful arc that perfectly frames a curved glass facade or wraps seamlessly around an automotive chassis. That's the power of aluminum extrusion bending - a metalworking technique that shapes extruded aluminum profiles and tubes into complex, curved forms while preserving their structural integrity.
Whether you're a design engineer sketching your next architectural masterpiece or a fabrication specialist optimizing production workflows, understanding this process bridges the gap between creative vision and manufacturing reality. Bending aluminum isn't simply about applying force to metal. It's about managing the tension, compression, and torsion that occur simultaneously during the forming process.
Unlike bending raw sheet metal or bar stock, working with extruded profiles presents distinct challenges and opportunities. Extruded aluminum arrives with a consistent cross-sectional shape created by forcing heated billets through precision dies. This manufacturing origin gives the material predictable properties - but also means you're curving a profile that must maintain its designed geometry throughout the bend.
Aluminum's natural ductility makes it well-suited for bending applications. The material can undergo significant deformation without fracturing, and its low work hardening rate means less springback and improved dimensional accuracy compared to many alternatives. However, the bending process imparts immense stress onto the workpiece, potentially causing issues ranging from minor wall thinning to unacceptable defects like buckling or cracking.
When executed with proper technique, aluminum profile bending preserves the extrusion's structural integrity without compromising its strength - eliminating the need for welding or joining multiple components while reducing production costs.
Curved aluminum extrusion has become essential across diverse industries. In architecture and construction, bent profiles create striking facades, curtain walls, and structural elements where aesthetic curves meet engineering demands. The automotive sector relies heavily on aluminium extrusion bending for exhaust systems, chassis components, and safety structures. Aerospace manufacturers use these techniques for aircraft frames and wing components where every gram matters.
Before selecting a bending method, you'll need to consider three critical factors:
The sections ahead will guide you through comparing bending methods, calculating safe bend radii, troubleshooting common defects, and making cost-effective decisions for your specific application. You'll find actionable guidance whether you're specifying your first curved aluminum extrusion or refining an established production process.
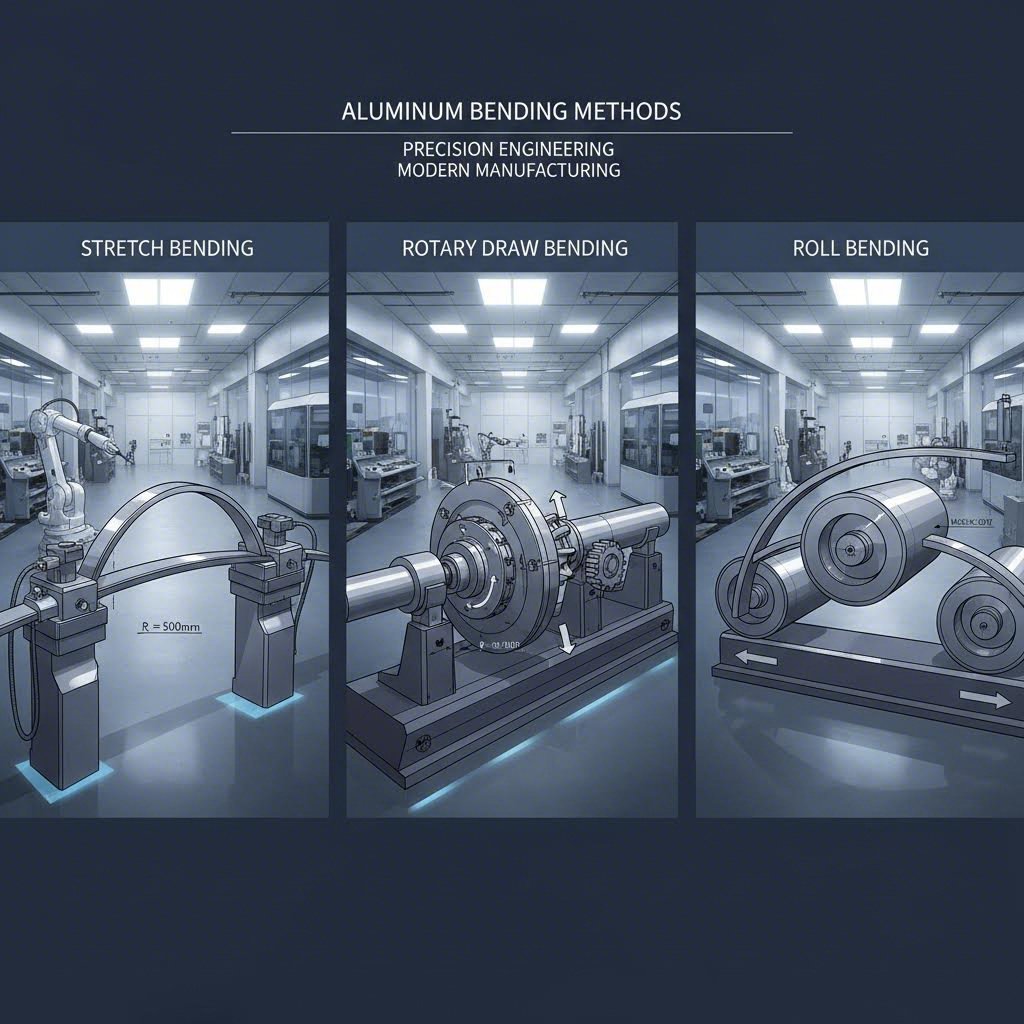
Choosing the right bending method can make or break your project. Each technique offers distinct advantages depending on your profile geometry, required radius, production volume, and quality specifications. Let's explore the six primary methods used in aluminium bending operations - and more importantly, when to use each one.
When your design calls for sweeping, large-radius curves, stretch bending delivers exceptional results. This method works by gripping both ends of the aluminum profile and applying tensile force while simultaneously wrapping it around a forming die. The simultaneous stretching and bending action distributes stress evenly across the workpiece, minimizing springback and virtually eliminating wrinkling on the compression side.
Stretch bending excels at creating architectural elements like curved curtain wall frames, stadium seating rails, and transportation applications requiring consistent, gentle arcs. The process handles both symmetric and asymmetric profiles effectively, though complex hollow sections may require internal support. You'll find this method particularly valuable when surface finish quality is paramount - the controlled tensile stress prevents the surface distortions common with other approaches.
Need tight radii with precision repeatability? Rotary draw bending is your answer. This technique clamps the aluminum tube or profile against a rotating bend die while a pressure die forces the material to conform to the die's radius. The controlled, consistent motion produces highly accurate bends with excellent repeatability - making it ideal for high-volume production runs.
Aluminum tube bending operations frequently rely on rotary draw methods for automotive exhaust systems, handrails, and furniture frames. The process accommodates centerline radii as tight as 1.5 times the tube diameter when combined with mandrel support. However, tooling costs run higher than simpler methods, so it's best suited for projects where precision justifies the investment.
Roll bending passes the profile through a series of three or four rollers, progressively curving the material with each pass. This method offers remarkable flexibility - you can create different radii without changing tooling simply by adjusting roller positions. It's particularly effective for producing large-radius curves, spirals, and even complete circles.
The trade-off? Roll bending typically leaves straight sections at each end of the workpiece where the rollers couldn't engage fully. For applications where every inch must be curved, you'll need to factor in additional material for trimming. Still, for bending aluminium extrusion into architectural rings, curved beams, or spiral staircases, roll bending remains the most economical choice.
Hollow aluminum profiles face a unique challenge: the unsupported interior walls can collapse or wrinkle during bending. Mandrel bending solves this by inserting a segmented internal support - the mandrel - inside the tube during forming. This internal support maintains the profile's cross-sectional shape through the bend zone.
You'll encounter mandrel bending frequently in aerospace tubing, hydraulic lines, and premium automotive applications where wall collapse is unacceptable. The method adds complexity and cost but delivers superior results for thin-walled tubes requiring tight radii.
Not every project demands sophisticated tooling. Ram bending uses a hydraulic or mechanical ram to push the profile against stationary wing dies, creating a bend at the contact point. It's fast, requires minimal tooling investment, and works well for less demanding applications with generous tolerance requirements.
Press bending operates similarly, using a press brake to form bends in aluminum profiles. Both methods suit lower-volume production, prototyping, or applications where slight surface marking and looser tolerances are acceptable. They struggle with complex hollow sections and tight radii but offer significant cost advantages for simpler geometries.
| Bending Method | Ideal Applications | Achievable Radius Range | Profile Complexity | Relative Cost |
|---|---|---|---|---|
| Stretch Bending | Architectural curves, large sweeps | Large to very large (8x+ diameter) | High - handles complex shapes | Medium-High |
| Rotary Draw Bending | Precision tubes, high-volume production | Tight to medium (1.5x-6x diameter) | Medium - best for tubes/simple profiles | High |
| Roll Bending | Variable radii, rings, spirals | Medium to very large | Medium - suits solid and hollow sections | Low-Medium |
| Mandrel Bending | Thin-wall tubes, aerospace components | Tight (1.5x-3x diameter) | Medium - hollow sections only | High |
| Ram Bending | Simple bends, prototyping | Medium to large | Low - simple profiles preferred | Low |
| Press Bending | Low-volume production, angular bends | Medium to large | Low - solid sections preferred | Low |
Your profile's cross-sectional geometry often dictates which bending method will succeed. Consider these key factors:
Understanding these relationships helps you specify profiles that are inherently more bendable - or select methods capable of handling challenging geometries. The next section explores how alloy selection and temper conditions further influence your minimum achievable bend radius.
Ever wondered why some aluminum bending projects succeed flawlessly while others crack at the first curve? The answer often lies in understanding minimum bend radius - that critical threshold where your material transitions from smooth deformation to sudden failure. Getting this calculation wrong means scrapped parts, delayed timelines, and frustrated customers.
The minimum bend radius represents the tightest curve you can achieve without compromising the material's integrity. Push beyond this limit, and you'll encounter cracking on the outer surface, excessive thinning, or complete fracture. Stay within safe parameters, and you'll produce bent aluminum components that maintain their strength and appearance.
Not all aluminum alloys bend equally. The two most common extrusion alloys - 6063 and 6061 - demonstrate notably different forming characteristics that directly impact your design decisions.
6063 Aluminum: Often called the "architectural alloy," 6063 offers superior bendability thanks to its lower magnesium and silicon content. This composition creates a more ductile material that flows smoothly during forming operations. You can typically achieve minimum bend radii of 1 to 2 times the material thickness for simple profiles in annealed condition. For curved aluminum extrusion in facades, window frames, and decorative trim, 6063 remains the preferred choice.
6061 Aluminum: This structural workhorse trades some formability for increased strength. Higher magnesium content makes 6061 more resistant to deformation - great for load-bearing applications, but demanding tighter process control during bending. Expect minimum bend radii of 2 to 3 times material thickness, with some temper conditions requiring even more generous curves. Automotive chassis components, aircraft structures, and marine applications frequently specify 6061 despite its reduced bendability.
5052 Aluminum: While less common in extrusion applications, 5052 aluminum bending deserves mention for sheet and plate work. This alloy offers excellent formability and corrosion resistance, making it suitable for marine and chemical processing environments where tight bends meet harsh conditions.
Here's where aluminum bending gets interesting - the same alloy can behave dramatically differently depending on its temper state. Think of temper as the material's "mood" during forming.
T4 Temper (Solution Heat Treated and Naturally Aged): This condition represents aluminum at its most cooperative. The material has been heat treated but hasn't yet reached full hardness, leaving it relatively soft and ductile. T4 temper allows for tighter bend radii and forgives minor process variations. Many fabricators prefer receiving extrusions in T4 condition, bending them, then allowing natural aging to develop full strength.
T6 Temper (Solution Heat Treated and Artificially Aged): Full strength comes at a cost. T6 represents the fully hardened condition where aluminum reaches peak mechanical properties - but minimum bend radius increases significantly. Attempting tight curves in T6 material often results in cracking on the tension side of the bend. You'll need to increase your bend radius by 50% or more compared to T4 specifications.
O Temper (Annealed): When extreme formability matters more than strength, annealed aluminum offers maximum ductility. This fully softened condition permits the tightest possible radii, though the material requires subsequent heat treatment to restore useful mechanical properties.
Successfully calculating your minimum bend radius requires evaluating multiple interacting variables. Consider these critical factors before finalizing your specifications:
One of the most impactful decisions you'll make involves timing - should you bend aluminium before or after the final heat treatment? Each approach offers distinct advantages.
Bending in T4 Condition (Before Full Aging): This strategy works beautifully when you need tight radii or complex curves. Request extrusions in T4 temper, complete all forming operations while the material remains cooperative, then allow natural aging to T6 properties over several weeks. Alternatively, artificial aging after bending accelerates the process. This approach minimizes cracking risk and allows tighter tolerances.
Bending in T6 Condition (After Full Aging): Sometimes logistics or production schedules demand working with fully hardened material. Success requires designing with more generous radii from the start. If tight curves are essential, consider localized annealing of the bend zone before forming, by re-aging to restore properties. This adds process steps but enables geometries otherwise impossible in T6.
When to Choose Each Approach: Opt for pre-aging bending when your design requires radii less than 3 times wall thickness or involves complex profile geometries. Choose post-aging bending when material handling logistics favor fully hardened stock or when gentle curves allow adequate forming margin. Many production facilities maintain both capabilities, selecting the optimal approach project by project.
Understanding these material science fundamentals positions you to specify achievable bend radii from the design phase - preventing costly surprises during fabrication. But even with perfect radius calculations, bending operations can introduce defects that compromise your finished components. The next section examines common problems and their solutions.
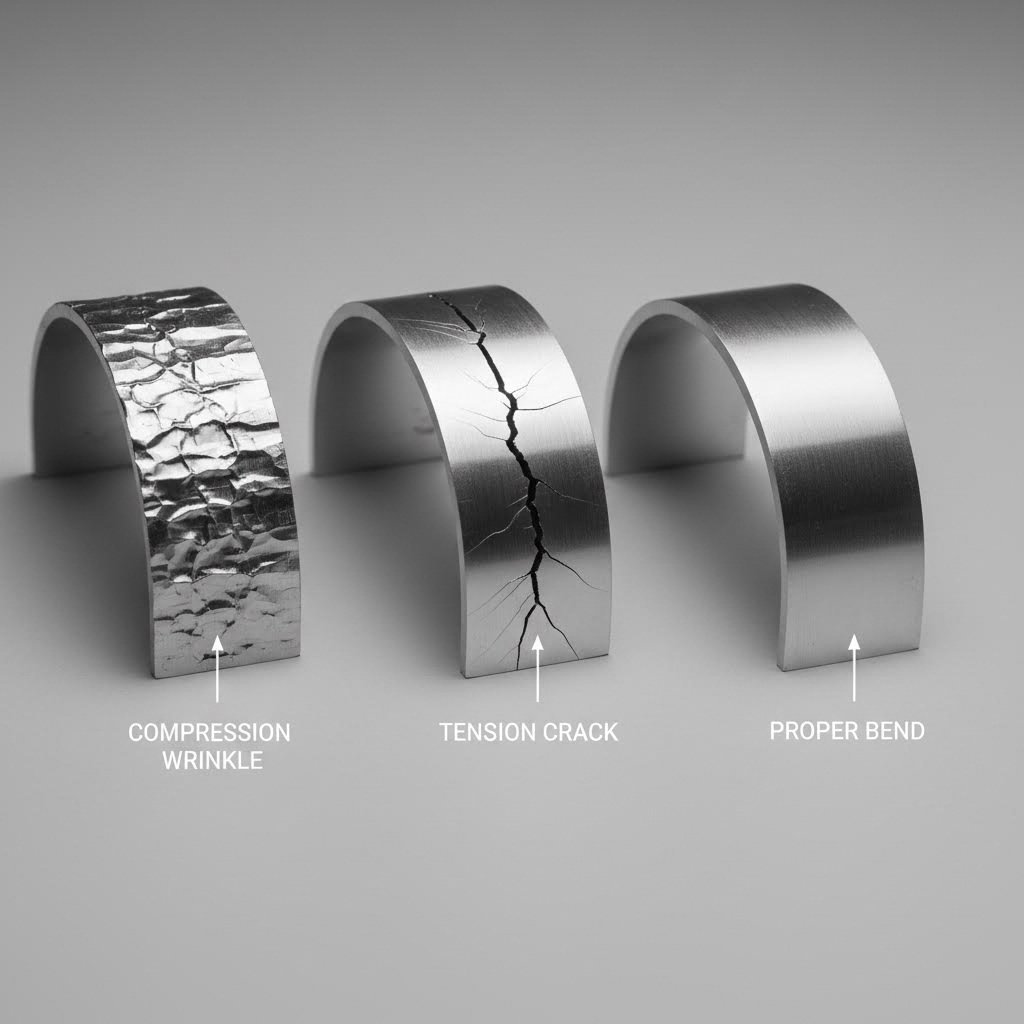
You've selected the right bending method and calculated your minimum radius - yet your curved extruded aluminum still shows wrinkles, cracks, or refuses to hold its intended shape. Sound familiar? Even experienced fabricators encounter defects that threaten part quality and production schedules. Understanding why these problems occur is the first step toward eliminating them.
Quality control in aluminium profile bending directly impacts safety, cost efficiency, and customer satisfaction. Poorly bent components can lead to structural failures, expensive rework, and missed deadlines. Let's examine the five most common defects and proven strategies for preventing each one.
When you bend aluminum, the inside of the curve experiences compression while the outside stretches in tension. That compression can cause the material to buckle and fold - creating unsightly wrinkles that compromise both appearance and structural integrity.
Wrinkling typically appears in thin-walled profiles, hollow sections without internal support, and bends with tight radii. The material essentially has nowhere to go as it's compressed, so it buckles like a drinking straw bent too sharply.
Prevention strategies include:
If wrinkling has already occurred, minor surface irregularities can sometimes be reduced through post-bend straightening operations. However, severe wrinkles typically require scrapping the part and adjusting process parameters for the next attempt.
Here's a frustrating scenario: your bend looks perfect coming off the machine, but the profile slowly relaxes back toward its original straight form. This elastic recovery - called springback - can throw your dimensions out of tolerance and require costly secondary operations.
Springback occurs because aluminum's elastic properties cause partial recovery after forming forces are released. Higher-strength alloys and tempers exhibit greater springback, as do profiles with larger cross-sections. The amount varies predictably based on material properties and bend geometry.
Controlling springback requires a proactive approach:
Experience with specific alloys and profile geometries helps fabricators predict springback accurately. Many shops develop compensation charts based on their equipment and typical materials, dialing in corrections before the first production bend.
Cracking represents the most serious bending defect - once material fractures, there's no recovery. Cracks typically initiate on the tension side of bends where material stretches beyond its ductility limit. Bending aluminum flat bar or solid profiles in fully hardened tempers frequently triggers this failure mode.
Surface distortion includes orange peel texture, die marks, and localized deformation that mar the finished appearance. These issues often stem from inadequate lubrication, worn tooling, or excessive forming speeds that don't allow material to flow smoothly.
Wall thinning occurs naturally as material stretches around the outside of curves. Some thinning is unavoidable, but excessive reduction weakens the profile and may violate design specifications. Tight radii, high stretch ratios, and thin starting walls all exacerbate this issue.
| Defect Type | Primary Causes | Prevention Methods | Correction Options |
|---|---|---|---|
| Wrinkling | Compression buckling, insufficient internal support, tight radius | Mandrel support, wiper dies, increased radius, stretch bending | Minor smoothing possible; severe cases require scrap |
| Cracking | Exceeding ductility limit, wrong temper, tight radius, surface defects | Softer temper, generous radius, localized annealing, defect-free stock | None - part must be scrapped |
| Springback | Elastic recovery, high-strength alloys, large cross-sections | Overbending, stretch bending, bottom coining, softer tempers | Re-bending to target angle, secondary straightening |
| Surface Distortion | Poor lubrication, worn dies, excessive speed, material handling damage | Proper lubrication, tooling maintenance, optimized parameters, protective films | Light polishing for minor marks; severe damage unrepairable |
| Wall Thinning | Excessive stretch, tight radius, thin starting wall, high bend angle | Generous radius design, thicker initial walls, reduced stretch ratio | None - design must accommodate acceptable thinning range |
Proper tooling selection prevents defects before they start. Match your die radius to the profile geometry, ensuring adequate support throughout the bend zone. Worn or damaged tooling transfers imperfections directly to your workpiece - implement regular inspection and replacement schedules.
Process parameters require equally careful attention. Bending speed affects material flow characteristics; too fast can cause tearing while too slow may allow unwanted deformation. Temperature matters for some applications - warming aluminum slightly increases ductility and reduces cracking risk on challenging geometries.
Continuous process monitoring enables real-time adjustments. Tracking parameters like pressure, angle, and temperature throughout each bend cycle helps identify drift before it produces defective parts. Statistical process control techniques allow manufacturers to detect variations and take corrective action proactively.
Different bending methods deliver different precision levels. Understanding achievable tolerances helps you specify appropriate methods for your quality requirements:
Tighter tolerances demand more sophisticated equipment, increased setup time, and often in-process measurement. Specify only the precision your application truly requires - over-specifying tolerances drives up costs without adding value.
With defect prevention strategies in place, your next consideration involves surface finishing - specifically, whether to apply treatments before or after bending operations.
Here's a question that trips up even experienced fabricators: should you apply that beautiful anodized finish before or after bending aluminum extrusions? Get the sequence wrong, and you'll watch your carefully curved profile develop cracks, discoloration, or coating failures that send parts straight to the scrap bin.
The relationship between surface treatments and bending operations isn't just about aesthetics - it directly impacts structural integrity, production efficiency, and final part quality. Different finishing types interact with the bending process in distinct ways, and understanding these interactions helps you plan smarter manufacturing sequences.
The golden rule? Bend first, finish second - at least for most applications. According to industry guidelines from Inductaflex, anodizing and powder coating are best applied after bending to prevent surface cracking or defects. The forming stresses that occur during bending aluminum extrusions can compromise coatings applied beforehand, leading to visible damage exactly where your curves are most prominent.
Why does sequence matter so much? During bending, the outer surface stretches while the inner surface compresses. Pre-applied coatings lack the flexibility to accommodate this deformation. Anodized layers - which become part of the aluminum itself through electrochemical conversion - are particularly brittle and prone to cracking under tensile stress. Powder coatings may chip, flake, or develop micro-fractures that compromise corrosion protection.
That said, some situations demand pre-finished material. When post-bend access is limited, when batch anodizing isn't economical for small quantities, or when specific color matching requires pre-coated stock, you'll need protective strategies to minimize forming damage.
When bending pre-anodized aluminium extrusion types becomes unavoidable, protective measures can reduce - though rarely eliminate - surface damage:
Even with these precautions, expect some degree of surface compromise on tight-radius bends. The anodic layer's inherent brittleness limits how much protection is achievable. For critical visual surfaces, post-bending finishing remains the recommended approach.
Each surface treatment has unique characteristics that influence optimal timing. Here's your decision guide:
Finishing after forming introduces its own requirements. Curved profiles need proper fixturing during coating processes to ensure complete coverage. Anodizing tanks and powder coating booths must accommodate the bent geometry without masking critical surfaces.
Pre-treatment remains essential regardless of timing. As noted by Comhan's technical resources, proper degreasing, rinsing, and conversion layer application ensures optimal adhesion between aluminum and any subsequent coating. Skipping pre-treatment steps risks peeling, uneven coverage, or premature coating failure.
For CNC aluminium extrusion operations requiring precision bends and premium finishes, coordinate closely with both your bending supplier and finishing house. Shared understanding of tolerances, handling requirements, and quality expectations prevents costly miscommunication.
With surface finishing strategy sorted, your next consideration involves the financial side of the equation - understanding what drives costs across different bending methods and production scenarios.
So you've identified the perfect bending method and calculated your ideal radius - but how much will this actually cost? Understanding the economics behind curved aluminum extrusions helps you make smarter decisions that balance quality requirements with budget realities. The difference between cost-effective method selection and expensive overkill often comes down to matching your specific project parameters with the right approach.
Unlike commodity manufacturing where prices follow predictable formulas, aluminum extrusion bending costs vary dramatically based on tooling requirements, production volumes, and profile complexity. A method that's economical for one project might prove prohibitively expensive for another - even when working with similar materials.
Four primary factors determine what you'll pay for curved aluminum extrusions. Understanding each helps you identify opportunities for optimization without sacrificing quality.
Tooling Investment: Custom dies represent your largest upfront expense. According to Profile Precision Extrusions, most custom extrusion dies fall between $1,250 and $1,950 depending on profile complexity. Bending tooling adds further investment - rotary draw dies can run several thousand dollars, while simple ram bending setups cost considerably less. The more intricate your design with features like multiple hollows, tight corners, or thin walls, the higher both extrusion and bending tooling costs climb.
Setup Time: Each bending operation requires machine setup, tool changes, and test runs before production begins. Complex profiles or tight tolerances demand longer setup periods and more trial pieces. CNC aluminum extrusion bending equipment reduces setup time for repeat orders but requires initial programming investment. Simple profiles on ram or press bending equipment set up quickly, while stretch bending or mandrel operations need more preparation.
Production Volume: Here's where economics get interesting. High tooling costs spread across thousands of pieces become negligible per-unit expenses. That same tooling investment on a 50-piece run, however, significantly impacts your piece price. Quantity discounts can reduce costs by up to 70% on larger orders, making volume planning crucial for budget optimization.
Profile Complexity: Your cross-sectional geometry directly influences pricing at every stage. Hollow sections requiring mandrel support cost more to bend than solid profiles. Asymmetric shapes may need specialized fixturing. Tight tolerances on curved aluminum extrusions demand additional inspection time and potentially slower production speeds.
Different bending approaches carry distinct cost profiles. This comparison helps you match methods to budget constraints:
| Bending Method | Tooling Investment | Per-Piece Cost (Low Volume) | Per-Piece Cost (High Volume) | Typical Lead Time |
|---|---|---|---|---|
| Ram Bending | $500 - $1,500 | $$ | $ | 1-2 weeks |
| Press Bending | $500 - $2,000 | $$ | $ | 1-2 weeks |
| Roll Bending | $1,000 - $3,000 | $$ | $ | 2-3 weeks |
| Rotary Draw Bending | $3,000 - $8,000 | $$$ | $$ | 3-5 weeks |
| Stretch Bending | $2,500 - $6,000 | $$$ | $$ | 3-4 weeks |
| Mandrel Bending | $4,000 - $10,000+ | $$$$ | $$ | 4-6 weeks |
Note: $ = lowest relative cost, $$$$ = highest relative cost. Actual pricing varies by supplier, location, and specific project requirements.
Smart cost management doesn't mean choosing the cheapest option - it means selecting the most appropriate method for your actual requirements. Ask yourself these questions:
Decision Framework for Cost-Effective Selection:
Working with your fabrication partner early in the design phase often reveals cost-saving opportunities. As noted by industry specialists, engaging during design helps "simplify profiles, select cost-effective tolerances, and avoid costly secondary machining." Sometimes minor design adjustments dramatically reduce bending costs without compromising function.
With cost considerations mapped out, your next step involves understanding the specific techniques required when bending hollow aluminum tubes - a specialty application with its own unique requirements and solutions.
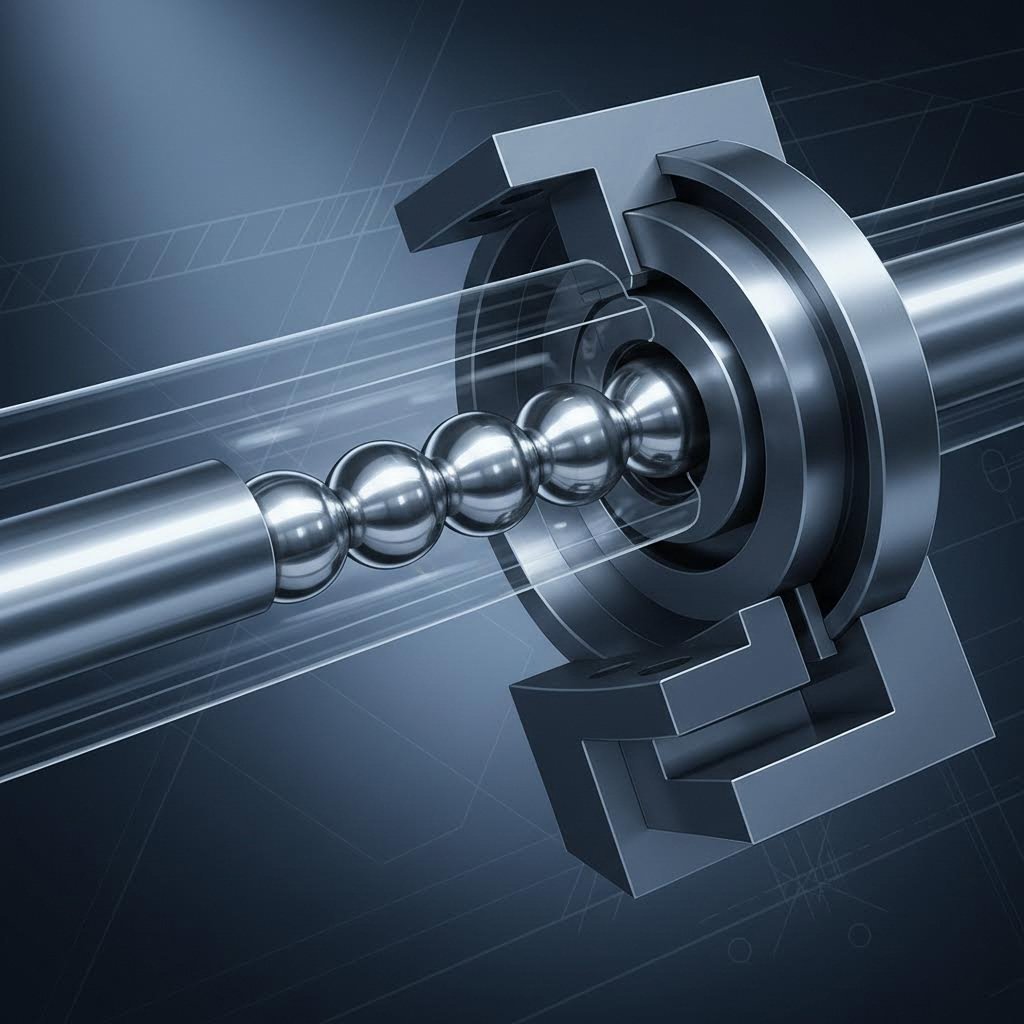
How do you bend aluminum tubing without ending up with a crushed, wrinkled mess? That's the challenge fabricators face when working with hollow aluminum profiles. Unlike solid extrusions that resist deformation through sheer material bulk, tubes and hollow sections have unsupported interior walls that can collapse, buckle, or distort the moment bending forces are applied.
The aluminum tube bending process demands specialized techniques that solid profile bending simply doesn't require. You're essentially fighting against the tube's natural tendency to flatten at the bend point while simultaneously managing the compression and tension forces acting on opposite sides of the curve. Master these techniques, and you'll produce hollow aluminum profile bending results that maintain full structural integrity.
The mandrel is your secret weapon against tube collapse. This internal support device fits inside the tube during bending, maintaining the cross-sectional shape through the critical bend zone where deformation forces peak.
Selecting the right mandrel involves two key calculations: the wall factor (tube outside diameter divided by wall thickness) and the "D" of bend (centerline radius divided by tube outside diameter). According to Bend Tooling's engineering guidelines, where these two measurements intersect on a mandrel-wiper chart determines your tooling requirements.
Here's how mandrel types break down:
The wall factor drives complexity. A tube with a wall factor of 15 (for example, 1.5" OD x 0.100" wall) bends more easily than one with a wall factor of 40 (1.5" OD x 0.0375" wall). Higher wall factors - meaning thinner walls relative to diameter - demand more sophisticated mandrel support.
Thin-walled aluminum tubes represent the most challenging hollow aluminum profile bending scenarios. Without proper support, these sections collapse on the inside of the bend while wrinkling develops on the compression side. The result? Rejected parts and wasted material.
Wiper dies work alongside mandrels to prevent wrinkling. Positioned just behind the bend die, wipers smooth the material flow on the compression side, preventing buckles from forming as material bunches up during the bend. For demanding applications, both mandrel and wiper become essential.
According to tube bending specialists at E Tube and Wire, thin-walled tubes require extra precautions: "Avoid overloading them during bending. Thin-walled tubes are more susceptible to deformation, so use proper support and mandrels to maintain their shape."
Additional strategies for thin-wall success include:
Whether you're setting up a production run or tackling a prototype, following a systematic approach ensures consistent results. Here's the proven sequence:
Achieving tight radii on hollow profiles without compromising structural integrity requires careful balance. The general rule - minimum bend radius equals approximately 2 times the outside diameter for aluminum tubes - assumes adequate wall thickness and proper tooling.
When pushing toward tighter curves, consider these factors:
For applications requiring extremely tight radii, consider heat-assisted bending. Warming the aluminum slightly increases ductility, though this adds process complexity and may affect temper properties. Alternatively, specifying T4 temper stock instead of T6 allows significantly tighter curves without the cracking risk associated with fully hardened material.
Understanding these tube-specific techniques positions you to tackle hollow aluminum profile bending with confidence. But successful execution also depends on having the right equipment - and that's where CNC capabilities and proper press tonnage become critical factors in achieving precision results.
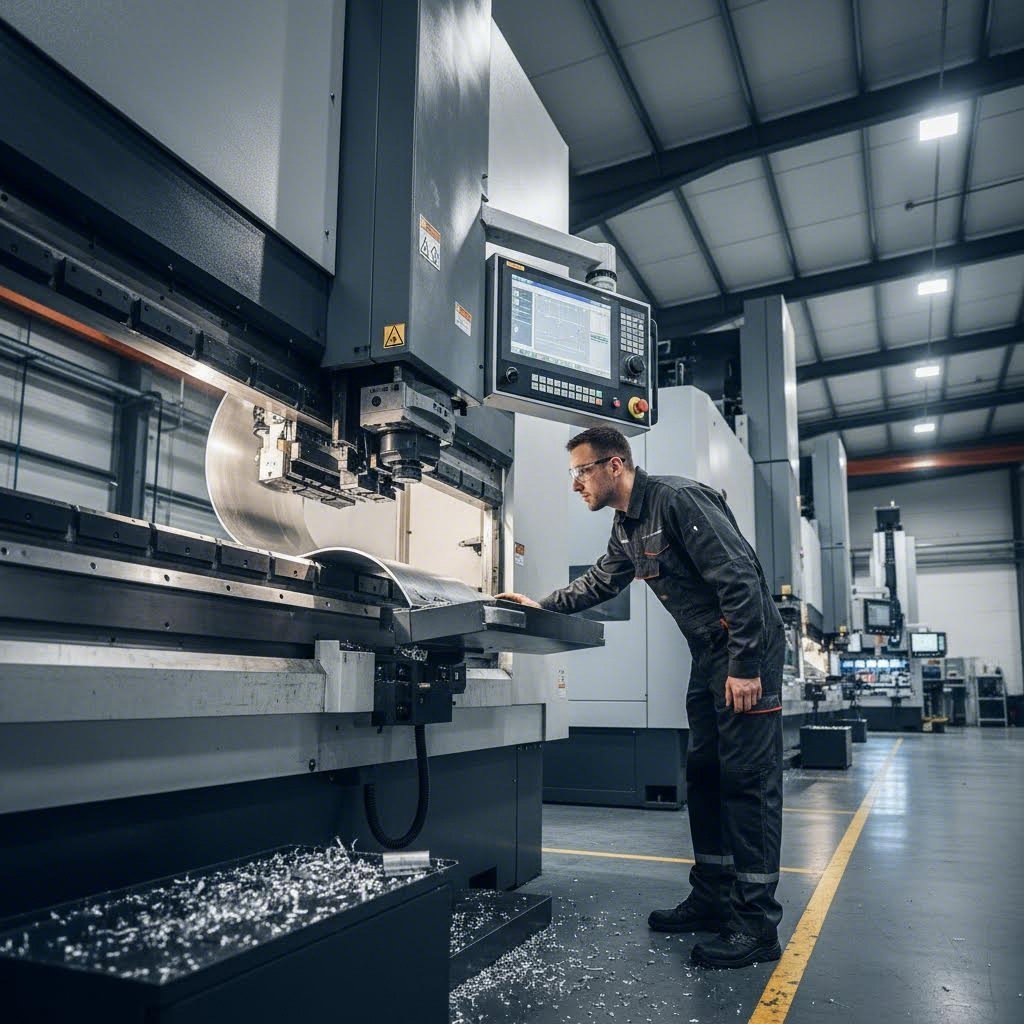
You've mastered the techniques and understand the material science - but without the right equipment, even perfect planning falls short. The machinery behind aluminum extrusion bending has evolved dramatically, with CNC aluminum bending equipment now delivering precision that manual operations simply cannot match. Understanding what equipment capabilities your project demands helps you select partners who can actually deliver your specifications.
Modern precision aluminum extrusion tooling integrates computer control, hydraulic power, and sophisticated sensing systems to produce repeatable results across thousands of pieces. Whether you're prototyping a handful of curved profiles or running production volumes in the tens of thousands, matching equipment capabilities to project requirements determines your success.
Computer numerical control has transformed aluminum profile processing equipment from skilled-operator-dependent machines into precision manufacturing systems. According to VPIC Group's CNC bending analysis, CNC machines automate the bending process by using a computer to control the machinery and hydraulic system, shaping components with more consistent bends and exact dimensions.
What does this mean for your curved aluminum extrusions? Three critical advantages:
CNC machining centers extend beyond bending alone. These integrated systems perform precise cutting, drilling, milling, and bending operations - often completing complex aluminum profiles in a single setup. This consolidation reduces handling damage, eliminates tolerance stack-up between operations, and accelerates production timelines.
The efficiency gains are substantial. As noted in industry analyses, each CNC bending process requires only one machine rather than multiple steps across different equipment. Fewer laborers are needed, and the consistency of automated machinery removes the need for manual fixes that would otherwise slow production.
Industrial bending machinery comes in vastly different capacities - and selecting inadequate tonnage leads to incomplete bends, machine damage, or both. Press tonnage measures the force available to deform your aluminum profile, and proper matching prevents costly problems.
According to Hunsone's press brake selection guide, several variables influence required tonnage:
The relationship follows a simplified formula: Tonnage = (575 x Thickness² x Length) / Die Opening, where thickness and die opening are in millimeters and length in meters. For a 3mm thick, 1 meter long aluminum section with a 30mm die opening, you'd need approximately 5 tons of force - though actual requirements vary with alloy and profile geometry.
Selecting the correct press brake tonnage ensures safety, accuracy, and efficiency while avoiding unnecessary costs from oversized equipment.
Your project scale and complexity determine the equipment specifications you should seek from potential fabrication partners. Here's how different project types align with equipment needs:
For projects demanding comprehensive capabilities, manufacturers with extensive equipment ranges offer significant advantages. Shengxin Aluminium's processing facilities, for example, house 35 extrusion presses ranging from 600T to 5500T alongside CNC machining centers - enabling them to handle everything from delicate architectural trim to heavy structural profiles within a single production environment.
Before committing to a fabrication partner, evaluate their equipment against your specific requirements:
The integration between extrusion and bending operations deserves special attention. Facilities offering end-to-end processing - from die development through extrusion, bending, and surface finishing - eliminate the coordination challenges and tolerance accumulation that occur when multiple vendors handle different process stages.
With equipment capabilities understood, you're ready to evaluate potential partners holistically - considering not just their machinery, but their experience, quality systems, and ability to support your project from initial design through final delivery.
You've absorbed the technical knowledge - bending methods, alloy behavior, defect prevention, and equipment requirements. Now comes the decision that brings it all together: choosing the right aluminum extrusion fabrication partner. This final step often determines whether your project succeeds smoothly or struggles through costly revisions and delays.
Finding a professional aluminum bending supplier isn't simply about comparing quotes. According to Profile Precision Extrusions, the right partner brings tangible benefits including increased efficiency, cost reduction, improved product quality, and scalability that grows with your needs. The wrong choice leads to inconsistent quality, delayed deliveries, and the frustration of misaligned expectations.
What separates exceptional custom aluminum bending services from mediocre ones? Start by asking these critical questions before committing to any supplier:
Technical capabilities matter enormously, but so does communication. The best fabricators provide progress updates, engineering feedback, and timeline reviews throughout your project. This partnership approach ensures alignment from initial design through final delivery.
Successful aluminum extrusion bending projects share common characteristics: thorough planning, appropriate method selection, and partners with end-to-end capabilities. Here's your comprehensive checklist for project planning:
When evaluating potential partners, prioritize those offering comprehensive capabilities from die development through mass production. This integrated approach - where extrusion, bending, machining, and finishing happen under coordinated control - eliminates the communication gaps and quality variations that plague multi-vendor supply chains.
Consider what comprehensive aluminum profile manufacturing support looks like in practice. Shengxin Aluminium exemplifies this model with over 30 years of industry experience, 35 extrusion presses ranging from 600T to 5500T, and CNC machining centers for precise cutting, drilling, and bending. Their surface treatment options - including Anodizing in custom colors, Powder Coating, PVDF, and Micro-arc Oxidation - demonstrate the post-bending finishing capabilities that complete your curved profiles to specification.
This factory-direct approach to custom aluminum extrusion and bending services offers several advantages:
Your curved aluminum extrusion project deserves a partner who understands every aspect of the process - from the metallurgical behavior of 6063 alloy during forming to the equipment specifications that ensure precision results. With the knowledge you've gained throughout this guide, you're now equipped to ask the right questions, evaluate capabilities critically, and select a partner positioned to transform your design vision into flawless curved reality.
Successful aluminum tube bending requires internal support using mandrels - segmented devices inserted inside the tube during forming. Select your mandrel type based on wall factor (OD divided by wall thickness) and bend radius. Thin-walled tubes need ball mandrels with multiple segments, while heavier walls may only require plug mandrels. Wiper dies positioned behind the bend die prevent wrinkling on the compression side. Proper lubrication, optimized bending speed, and pressure die assist further prevent collapse and maintain cross-sectional integrity through tight curves.
Six primary methods dominate aluminum extrusion bending: stretch bending for large-radius architectural curves with minimal springback; rotary draw bending for tight, precision radii in high-volume production; roll bending for variable radii and complete circles; mandrel bending for hollow sections requiring internal support; ram bending for simpler, less demanding applications; and press bending for low-volume angular bends. Each method offers distinct advantages based on profile geometry, required radius, production volume, and tolerance specifications.
Minimum bend radius depends on multiple interacting variables: alloy type (6063 bends tighter than 6061), temper condition (T4 allows tighter curves than T6), wall thickness (thicker sections need larger radii), profile geometry (hollow sections require more generous curves), bend angle (90-degree bends stress material more), and grain direction. Generally, 6063-T4 achieves radii of 1-2 times material thickness, while 6061-T6 requires 2-3 times or more for safe bending without cracking.
The recommended approach is bend first, finish second. Anodizing creates brittle oxide layers that crack under bending stress, while powder coatings may chip or flake at bend points. Post-bending application of anodizing, powder coating, PVDF, and wet paint ensures uniform coverage and prevents surface damage. When pre-finished material is unavoidable, increase bend radius significantly, apply protective films, use soft-faced dies, and reduce bending speed to minimize coating damage.
Costs vary based on four primary factors: tooling investment (ranging from $500 for ram bending to $10,000+ for mandrel bending), setup time, production volume, and profile complexity. Low-volume projects benefit from simpler methods despite higher per-piece costs, while high-volume runs justify sophisticated tooling investments. Quantity discounts can reduce costs by up to 70% on larger orders. Working with partners offering end-to-end capabilities from extrusion through finishing, like Shengxin Aluminium with their 35 presses and CNC machining centers, often provides cost advantages through streamlined production.


 خدمة الإنترنت
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 العربية
 English
 français
 Deutsch
 русский
 español
 português
 ไทย
 Việt
 Українська