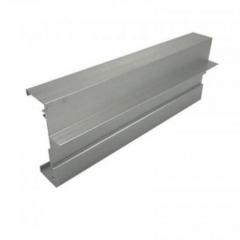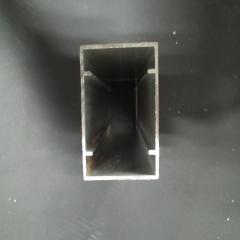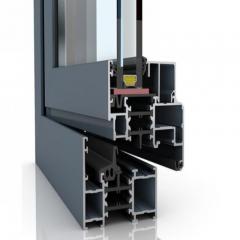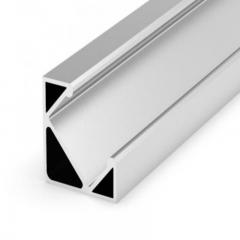
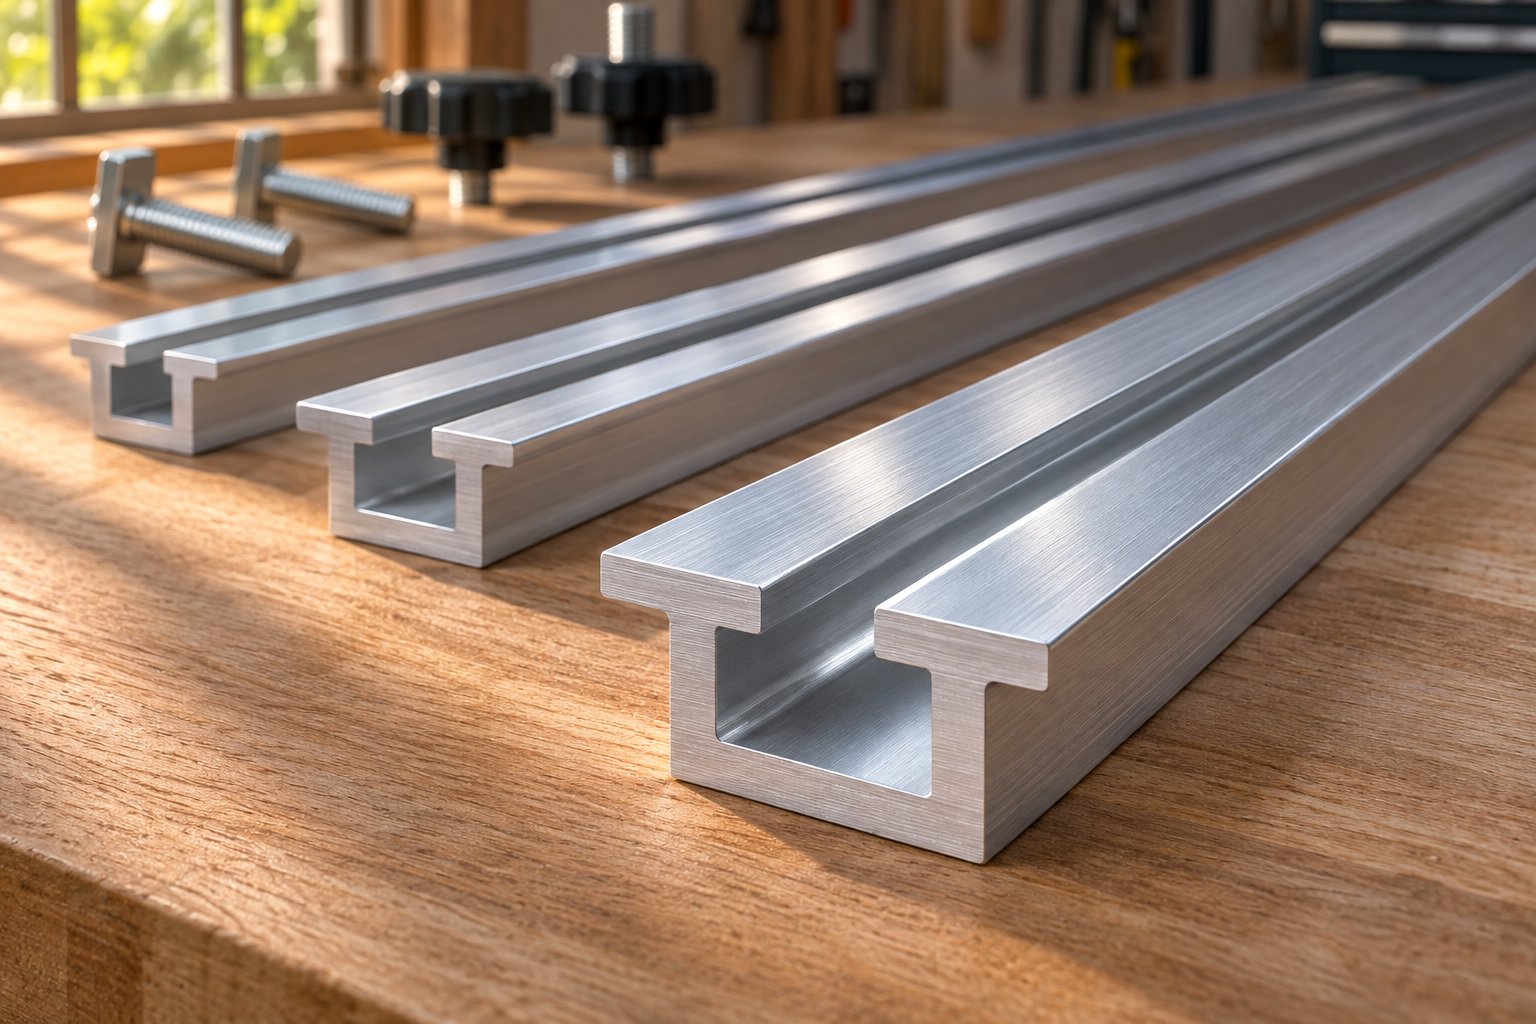
Aluminium T-track extrusions are aluminum profiles with one or more T-shaped slots running their full length. You slide a T-bolt, T-nut, or other sliding hardware into the slot, move it to any position, and tighten it to lock a fence, clamp, bracket, or panel in place. The slot has a narrow opening at the surface and a wider cavity underneath. The narrow opening keeps the fastener head from pulling out, and the wider cavity lets it slide freely until you clamp it down.
If you have ever moved a fence on a router table and locked it in place without drilling a new hole, you have used this slot. Plain rectangular tubing and basic channel stock only give you flat walls to drill through. A T-track gives you a mounting point along its whole length.
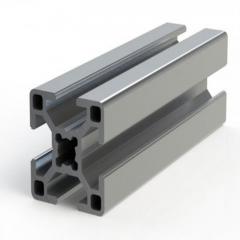
A slim aluminum t track set into a workbench and the square t slotted aluminum extrusions used in machine frames have the same basic parts:
The overall shape ranges from a low, single-channel track to square sections with a slot on every face. The dimensions are held to tight limits. Xometry notes that T-slot profiles usually follow Aluminum Association standards, with tolerances of about +/- 0.005 to +/- 0.015 inches depending on profile size.
A U-channel is a flat base with two legs. A C-channel adds lips to the ends of those legs for extra stiffness. Both are useful aluminum extrusions, but neither is designed to hold a fastener head captive while it slides. To mount something, you drill a hole. To move it, you drill another one.
A T-slot holds the fastener head, so you can skip the drilling. Hardware goes where you need it today and moves when the job changes tomorrow. That flexibility is why extruded aluminum framing shows up in everything from industrial machine frames to woodworking jig tables.
It also makes the profile unforgiving. If the slot is off by a fraction of a millimeter, hardware either binds or wobbles. Catalogs from framing brands and custom extruders such as BRT Extrusions Inc may list the same nominal slot sizes, but the real fit depends on how each aluminum extrusion was made, starting with the steel die that shapes it.
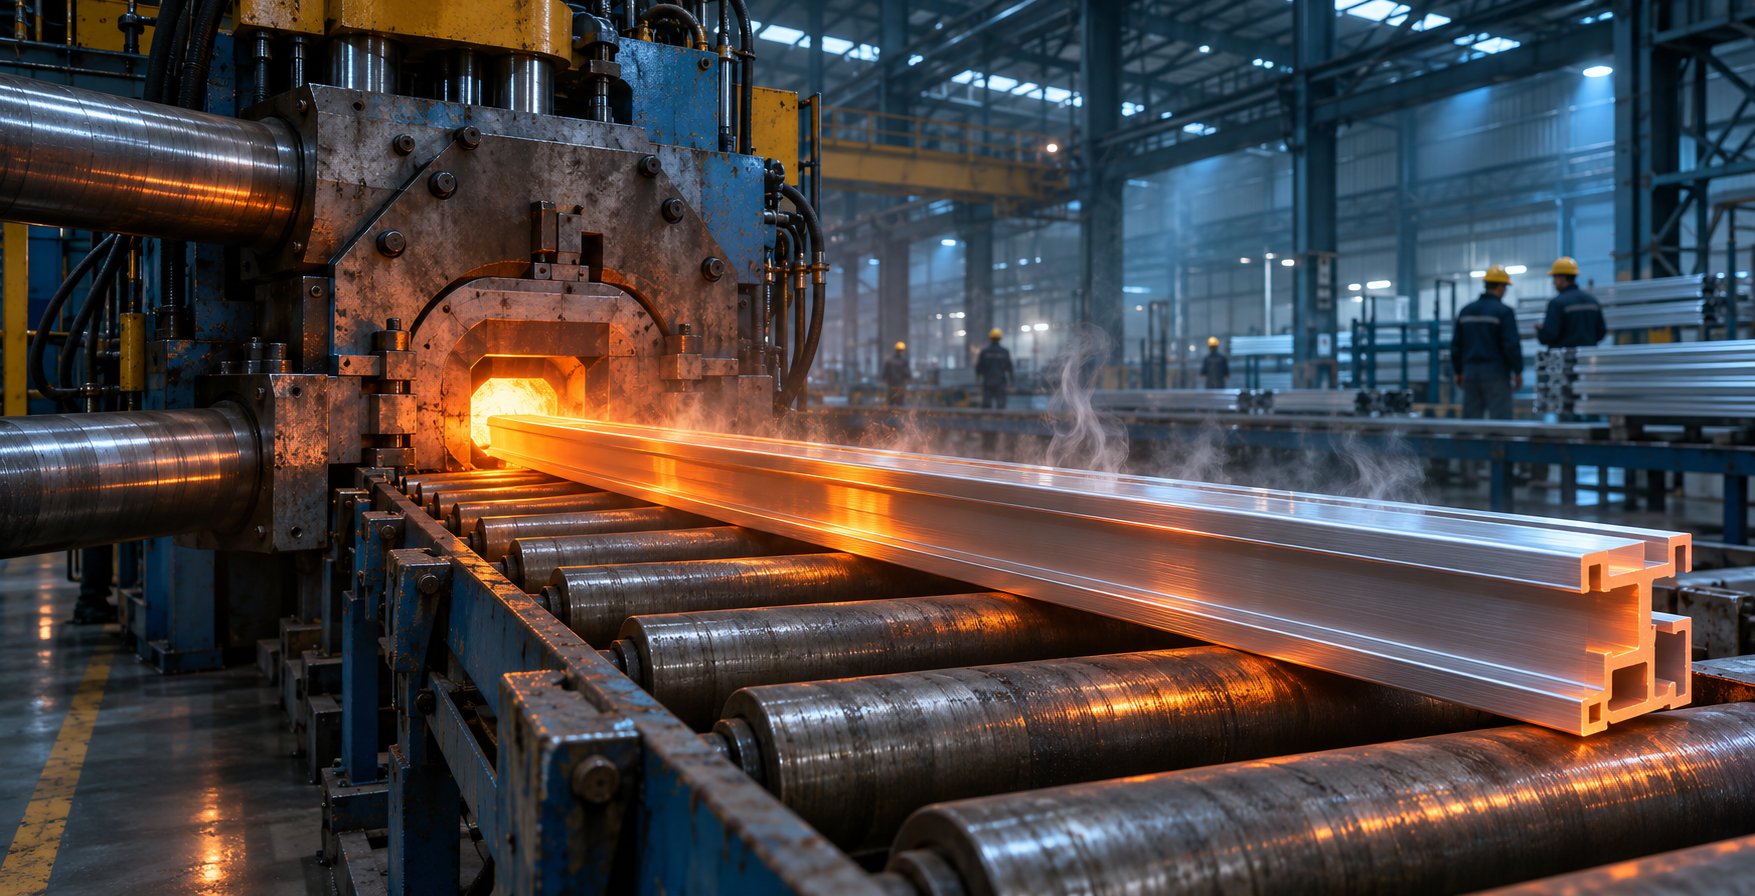
Why do two profiles sold under the same series number feel different when you slide a T-nut through them? Most of the answer lies in how each one was made. Every piece of extruded aluminum starts as a solid log of metal. A few production choices along the way decide how accurate, strong, and smooth the finished slot will be.
The Aluminum Extruders Council compares extrusion to a Play-Doh press. Soft material is pushed through a shaped opening and comes out in that shape. For T-track, the sequence looks like this:
The die sets every dimension of the profile, including the slot opening, cavity depth, flange thickness, and outer size. Profiles with a hollow core, such as square framing sections with a center bore, need a hollow die. Inside that die, a mandrel splits the metal flow, and the two streams weld back together under pressure. If a die is worn or poorly designed, the slot drifts out of tolerance, and the T-nuts start to bind. This is also why a 25 series extrusion and a 10 series profile can have similar outer dimensions and still take different hardware. Each series comes from its own die with its own slot geometry.
The alloy is still fairly soft when it leaves the press. It gets its working strength from aging, and the temper code tells you how that aging was done:
For 6063 alloy, T6 reaches an ultimate tensile strength of 35 ksi, compared with 27 ksi for T5. The rapid quench can also leave internal stresses that distort thin or complex sections, while T5 holds its shape better. On a detailed slot profile, accurate geometry can matter more than the extra strength.
The finish is applied last. It affects how well the profile lasts and how smoothly hardware slides in the slot:
On a shelf, two t slot rails can look identical and still differ in die quality, temper, and finish. The same press process also produces t-slot profiles for very different jobs, from four-sided framing to V-slot motion rails to low-profile track for jigs. The shape cut into the die decides which job a profile can do.
Search for T-track and you will see three kinds of results: square framing bars, grooved rails fitted with wheels, and slim tracks screwed into workbenches. All three have a T-shaped slot. Each one was designed for a different job, though. If you buy the wrong family, the hardware you planned around may not fit, or the profile may not handle the load you put on it.
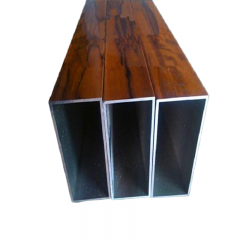
T slot aluminum framing uses square or rectangular profiles, often with a slot on all four faces. These profiles bolt together into rigid frames, enclosures, workstations, and machine bases. Joints are made with T-nuts and internal corner brackets, or with external gussets, so no welding is needed. In this family, the extrusion carries the load. If you need t slot aluminum to hold up a machine, this is the family to look at.
V-slot profiles keep the slot, but the edges of each opening are shaped into a V-groove. Wheels with a matching V-shaped rim ride in that groove, so the extrusion works as a frame member and a linear guide at the same time. The shop team at Interrobang names CNC machines, 3D printers, and linear motion systems among the most common uses. Because the slot still accepts nuts and brackets, one rail can hold the frame together and carry a moving gantry.
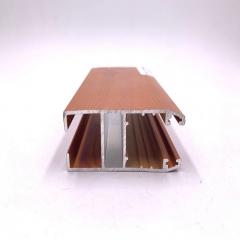
Dedicated T-track is a single-channel strip mounted on the surface of workbenches, router tables, and crosscut sleds. It is not designed to carry structural loads. Its job is to lock stops, fences, and hold-down clamps wherever you set them. POWERTEC describes Universal T-Track as a size shared by most makers. It accepts 5/16 in. and 1/4 in. T-bolts as well as 1/4 in. hex bolts, and it mounts in a dado routed into 3/4 in. board. Heavy-duty or mini track is not standardized across brands. It takes 1/4 in. hex bolts but not standard T-bolts, and it may need a larger dado and a thicker base.
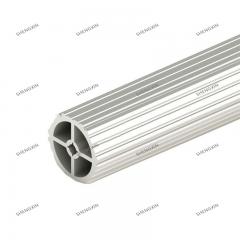
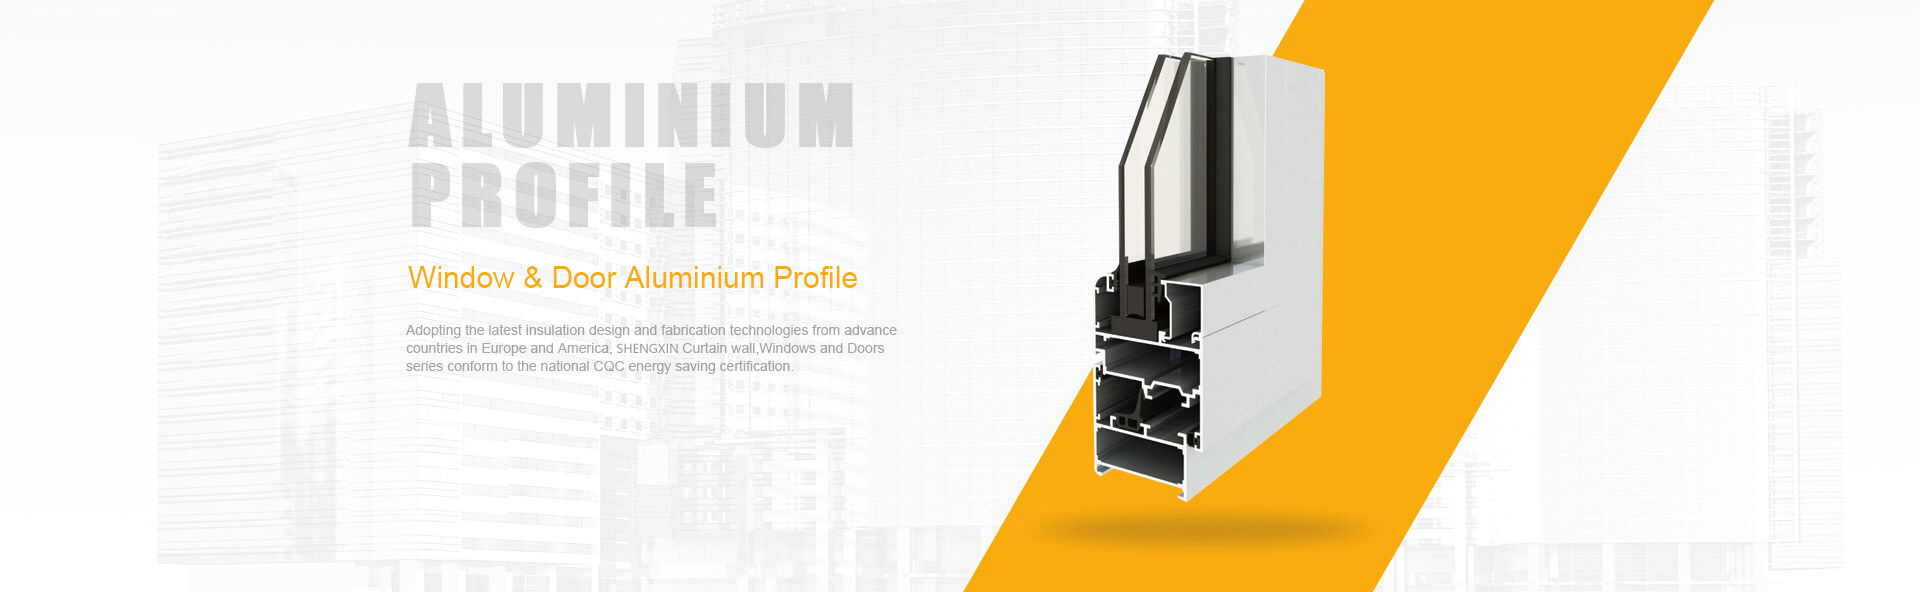
Some aluminum extrusion profiles combine features from more than one family. Shengxin Aluminium's 2020 T-track and V-slot profile puts both geometries in a single anodized 2020-series extrusion. The listing does not include a detailed slot drawing or a hardware compatibility chart. Confirm that your T-bolts, clamps, and rollers fit before you specify it.
| Profile Type | Slot Geometry | Typical Cross-Section Size | Primary Use Case | Compatible Hardware |
|---|---|---|---|---|
| Hybrid V-slot/T-track (example: Shengxin 2020 profile) | V-groove edges with a T-slot cavity. Detailed slot dimensions are not published. | 20 x 20 mm | Light frames that also carry rollers or fixtures | 2020-series T-nuts, V-wheels, and clamps. Test-fit before ordering. |
| Structural T-slot framing | T-slots on one to four faces, often with a center bore | Metric from 20 x 20 mm to 45 x 45 mm and larger. Fractional in 1 in. and 1.5 in. bases. | Frames, enclosures, machine guarding, and machine bases | T-nuts, bolts, internal corner brackets, gussets, and panel clips |
| V-slot linear motion | T-slot with a V-shaped groove along the opening | Built on a 20 mm module, such as 20 x 20, 20 x 40, and 20 x 80 mm | CNC routers, 3D printers, and linear axes | V-wheels, eccentric spacers, T-nuts, and gantry plates |
| Dedicated T-track | Single low-profile T-channel in universal or mini/heavy-duty sizes | Narrow strip sized for a routed dado. Universal track fits 3/4 in. board. | Jigs, fences, stops, and hold-downs | 1/4 in. and 5/16 in. T-bolts, 1/4 in. hex bolts, knobs, and flip stops |
All of these profiles come from the same kind of aluminum profile extrusion process, so the photos in a catalog can look alike. An extruded t slot in a 2020 rail and the slot in a 1.5 in. framing bar may look nearly identical on screen. They still take different T-nuts, and the series number printed next to each profile tells you which ones.
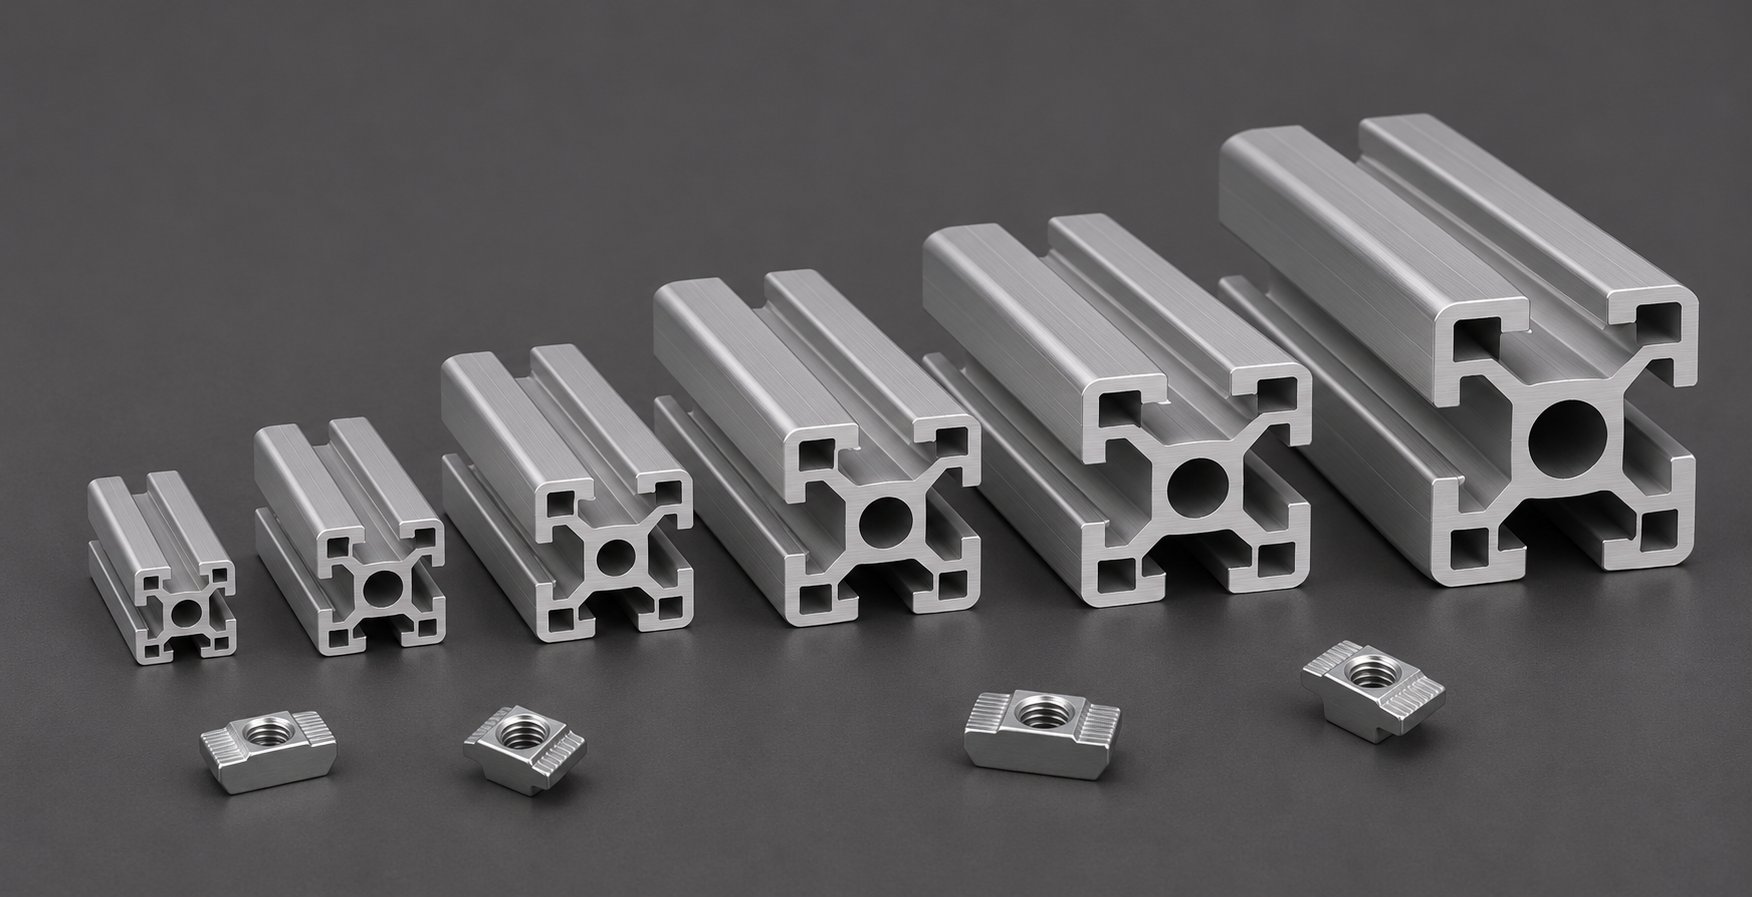
Open any T-slot catalog and you'll notice names like 1515, 20-2020, and 40-4080. These are size codes, not random part numbers. They come from two sizing systems, fractional inch and metric, and each series within a system has its own slot width. If you choose the series first, most of your hardware questions are already answered.
Fractional profiles are built on inch bases. In the 80/20 catalog, 10 series profiles start from a 1.00 in. square and 15 series profiles start from a 1.50 in. square. Larger shapes are multiples of those bases, such as the 1.50 x 3.00 in. 1530 or the 3.00 x 3.00 in. 3030. Framing Tech lists a 0.26 in. slot for 10 series and a 0.32 in. slot for 15 series. That difference is why T-nuts and brackets fit any profile in their own series but not profiles in another series.
The names can mislead you. The 80/20 naming guide points out that a 10 series 2020 measures 2 x 2 in. and has two slots per face, while a metric 20-2020 measures 20 x 20 mm and has one. The 25 series causes similar confusion. Its 25 mm base is about 0.98 in., so a 25-2525 looks almost like a 1010. It is still a metric profile with its own slot, so 10 series hardware won't carry over. The 40 and 45 series are also metric, even though people often group them with the large inch profiles.
Metric series use 20, 30, 40, and 45 mm bases. Framing Tech lists a 6 mm slot for 20 series, 8 mm for 30 series, and 10 mm for 45 series. The 40 series comes in both 8 mm and 10 mm versions, so check the slot width as well as the series number. Metric is the standard outside the US and the usual choice for 3D printer and hobby CNC builds. In the US, inch series are more common. The two systems are not interchangeable. If you combine extruded aluminium rails from an inch supplier with metric brackets, the parts will not fit.
As a starting point, match the series to the size of the project:
Load capacity also depends on span length and on how the joints are made, so check the supplier's deflection data before you order. Larger series also cost more. A cheap t slot rail in the wrong series is never the aluminum extrusion t-slot best price, because you will end up buying every T-nut and bracket a second time.
Choosing the right series makes the hardware fit, but it tells you nothing about how much the frame will flex. Two extruded aluminum rails with identical slots can still differ in strength, depending on the alloy they were extruded from.
Say one spec sheet lists 6063-T5 and another lists 6061-T6. Which should you buy? Almost all t-slot aluminum profiles are made from 6000 series alloys. Taber Extrusions calls this the main alloy family for extrusions. Its magnesium and silicon content makes it extrude easily, gives it good strength, and helps it resist corrosion. Three grades in this family cover most T-slot and T-track work.
6063-T5 is the most common choice. It flows easily through complex dies, so it holds sharp slot detail, and it takes anodizing well. Kloeckner Metals notes that 6063 contains almost no copper, so it resists corrosion better than other 6xxx alloys. Its strength is moderate. Taber says it is about half as strong as 6061. That is enough for frames, guarding, fixtures, and small aluminum extrusions such as woodworking jig track. You will see this grade most often on hardware-store track and generic metric framing.
Use 6061-T6 when a frame has to handle heavy dynamic loads, vibration, or impact. Kloeckner lists 6061 with a yield strength of about 276 MPa and a fatigue strength of 96.5 MPa. The figures for 6063 are 214 MPa and 68.9 MPa. 6061 also machines better. The drawback is that it has more copper, chromium, and silicon, so it does not flow through a die as easily. Fine slot features are harder to hold, and the profile usually costs more per foot.
6105-T5 falls between the other two grades. It is stronger than 6063 and extrudes more easily than 6061, so some framing brands specify it or the similar 6005-T5 for structural shapes. Vention, for example, extrudes its V2 profiles in 6005-T5 and rates them at 240 MPa yield strength. Whether you order online or search for t-slot profiles near me, look for the alloy and temper on the listing.
| Alloy | Typical Tensile Strength Range | Corrosion Resistance | Extrudability | Weldability | Common Use Cases |
|---|---|---|---|---|---|
| 6063-T5 | About 145 to 186 MPa | Excellent (A rating) | Excellent. Holds fine slot detail. | Good. Welding heat weakens the metal near the weld. | Light framing, guarding, jig track, and small profiles |
| 6061-T6 | Up to about 290 MPa | Good (B rating) | Fair. Fine features are harder to hold. | Good (A rating for gas and arc welding) | Frames that carry heavy loads or see vibration or impact |
| 6105-T5 | About 262 MPa (38 ksi) minimum | Good | Good. Easier to extrude than 6061. | Good. Welding heat weakens the metal near the weld. | Structural framing that needs more strength than 6063 |
The corrosion and weldability ratings above come from Kloeckner's Aluminum Association data. Welding an extruded aluminum t slot frame also gives up the main advantage of the system, which is that you can take it apart and rebuild it.
The alloy is only one part of the specification. Every alloy in the table has about the same stiffness. Vention uses a Young's modulus of 68,900 N/mm² for 6063-T5. Stiffness comes mostly from the cross-section. Vention tested two 45 x 45 mm profiles, each as a 500 mm cantilever under 1,500 N. One deflected 5.58 mm and the other 8.28 mm, because their cross-sections differed. A thin-walled 6061 profile can flex more than a thick-walled 6063-T5 one.
The alloy and temper set how much load the profile takes before it bends permanently. The cross-section sets how much it flexes under that load.
Compare alloy, temper, wall thickness, and moment of inertia together. The right combination depends on where the frame will be used. A machine base on a factory floor needs something different from a fence track in a garage workshop.
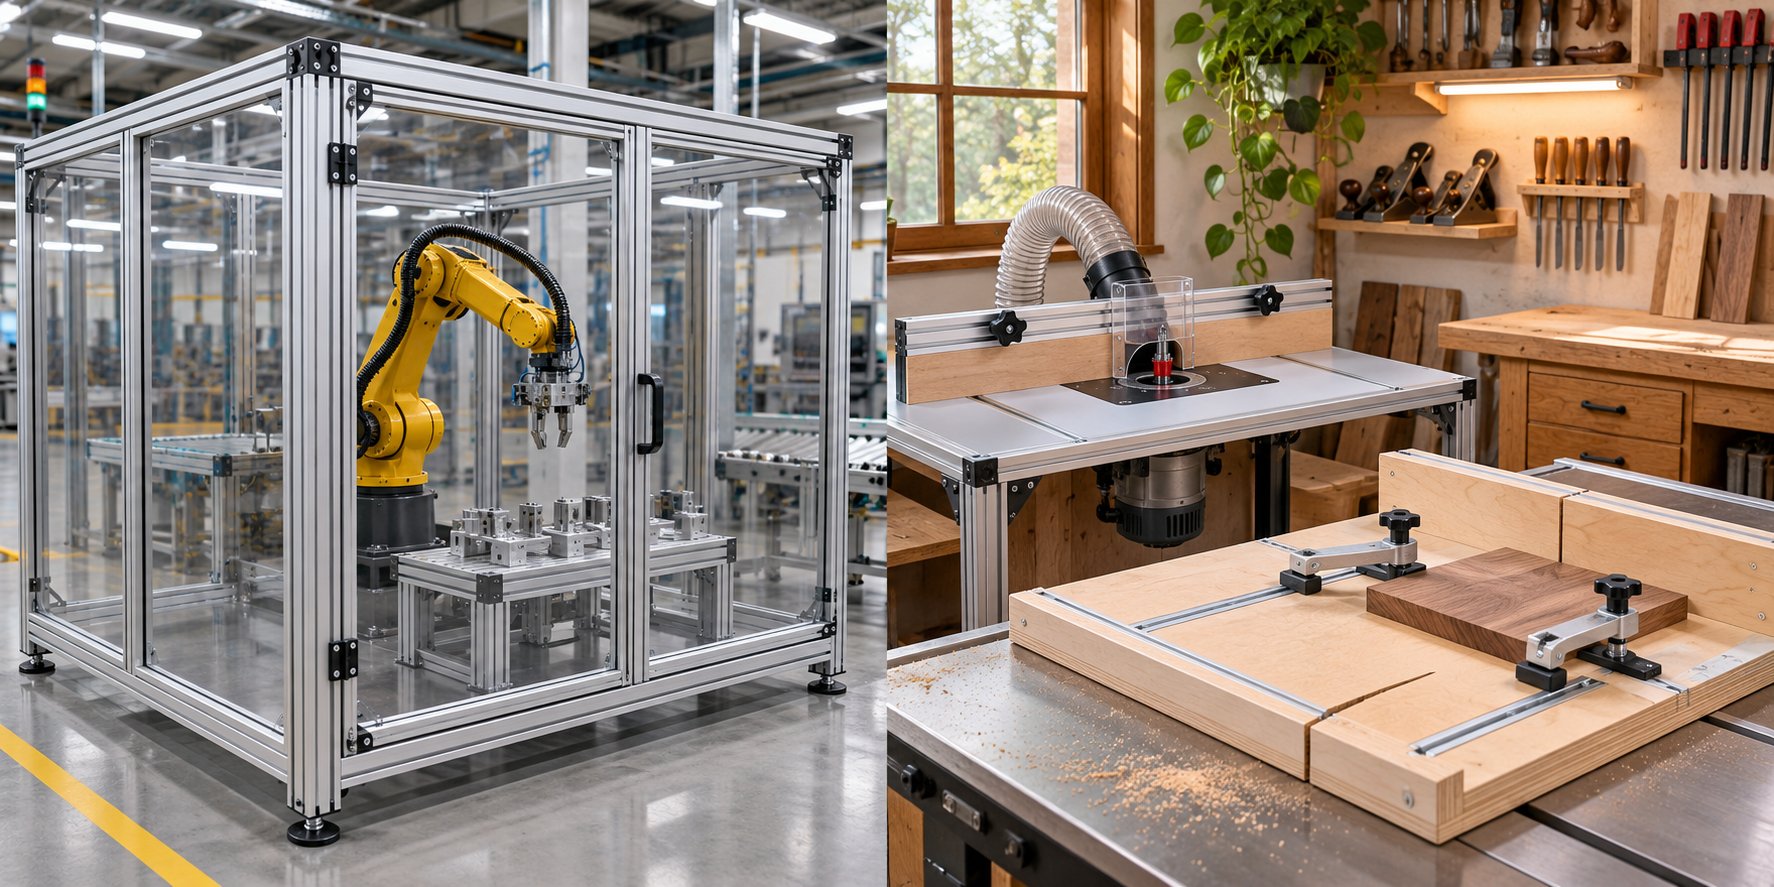
Who buys these profiles? A plant engineer guarding a robot cell and a woodworker building a crosscut sled might order from the same catalog page. Both depend on a slot that holds hardware anywhere along its length. The profile size, the alloy, and the way the extrusion is mounted are what change between the two jobs.
In a factory, the aluminum extrusion profile usually is the structure itself. Framing Tech lists custom workstations, machine guards, conveyor systems, and laboratory furniture among the most common uses. Machine guarding is a typical case. Polycarbonate panels sit in the slots of a 15 series or 40 mm frame, so operators can see the machine while the frame keeps their hands out of it. The same method is used for conveyor support frames, automated workstation structures, and equipment bases.
The main reason factories choose this system is that it can be rebuilt. When a production line changes, a crew loosens the T-nuts, moves the members, and bolts them back together. Nobody has to weld, cut a new weldment, or wait for a fabricator. Commercial users depend on the same property. Retail and trade show display frames are taken down and set up again in new layouts, and cleanroom partitions use the slots to hold wall panels.
Most makers who shop for extrusion aluminum want one of two things: a full machine frame or a track for jigs. For a frame, they use multi-slot structural profiles. In one Instructables build, a student used 20 x 20 mm extrusion for a CNC enclosure. He tapped M5 holes into the profile ends to join the pieces, friction-fit 1/4 in. MDF panels into the slots, and mounted the doors on hinges held by T-nuts so he could adjust their position.
For jigs, the standard approach is single-channel T-track set into MDF or plywood. WOOD magazine recommends clamping the track flush with the jig surface. Then you drill pilot holes through the track and into the jig, and countersink each hole until it matches the diameter of the screw head. The angled screw head pressing against the countersink is what holds the track down, so a slightly enlarged pilot hole does no harm.
Here is where each group typically uses these profiles:
Both groups use the same slot shape. A guarding frame is a 1.5 in. or 40 mm profile bolted to other profiles, often 6063-T5 or a stronger alloy in a larger series. A sled track is a slim 6063 strip screwed into wood. Neither one works without the parts that go into the slot. A fence track needs T-bolts that fit it, and a frame needs brackets and T-nuts to hold its members together. Choosing those parts is where many buyers make expensive mistakes with t-slot rails.
What actually holds a T-slot frame together? A bare length of extruded t slot aluminum is just a rail. T-nuts, bolts, and brackets turn it into a structure, and each of those parts is sized for one slot series.
Fasteners are usually labeled by the slot width they fit. Framing Tech uses its TN10M6 part as an example. It is a T-nut for the 10 mm slot found on 40 mm and larger metric profiles, and it has an M6 thread. You pick the slot width first, then the thread size that suits the part you're mounting.
The size has to match exactly. A T-nut made for a 6 mm metric slot won't seat properly in a 10 series slot. The 10 series opening is 0.26 in., only about 0.6 mm wider, but the cavity behind it is a different shape.
Connectors join the frame members:
All of these connectors fasten with T-nuts and bolts. You get a rigid three-dimensional frame with no welding and no permanent change to the profile.
When you mix suppliers, hardware compatibility matters more than anything else. A T-slot bracket guide from MKALU points out that no single published standard defines every dimension of every series. That makes "fits standard T-slot" marketing shorthand. Aluminum t slots with the same nominal size can still differ in depth and flange thickness. Before you order, check the slot width and depth on the t slot aluminium extrusion drawing against the fastener datasheet. The same applies to profiles you find by searching extruded aluminum home depot or a general marketplace. If the listing gives a shape and length but no slot width, ask for one.
Some connectors also need work on the profile itself. Airline lists M12 connecting screws and bolt connectors as needing an access hole or a pre-drilled hole. Hidden joints often need a thread tapped into the profile end. For those parts, you'll need to cut and drill the extrusion.
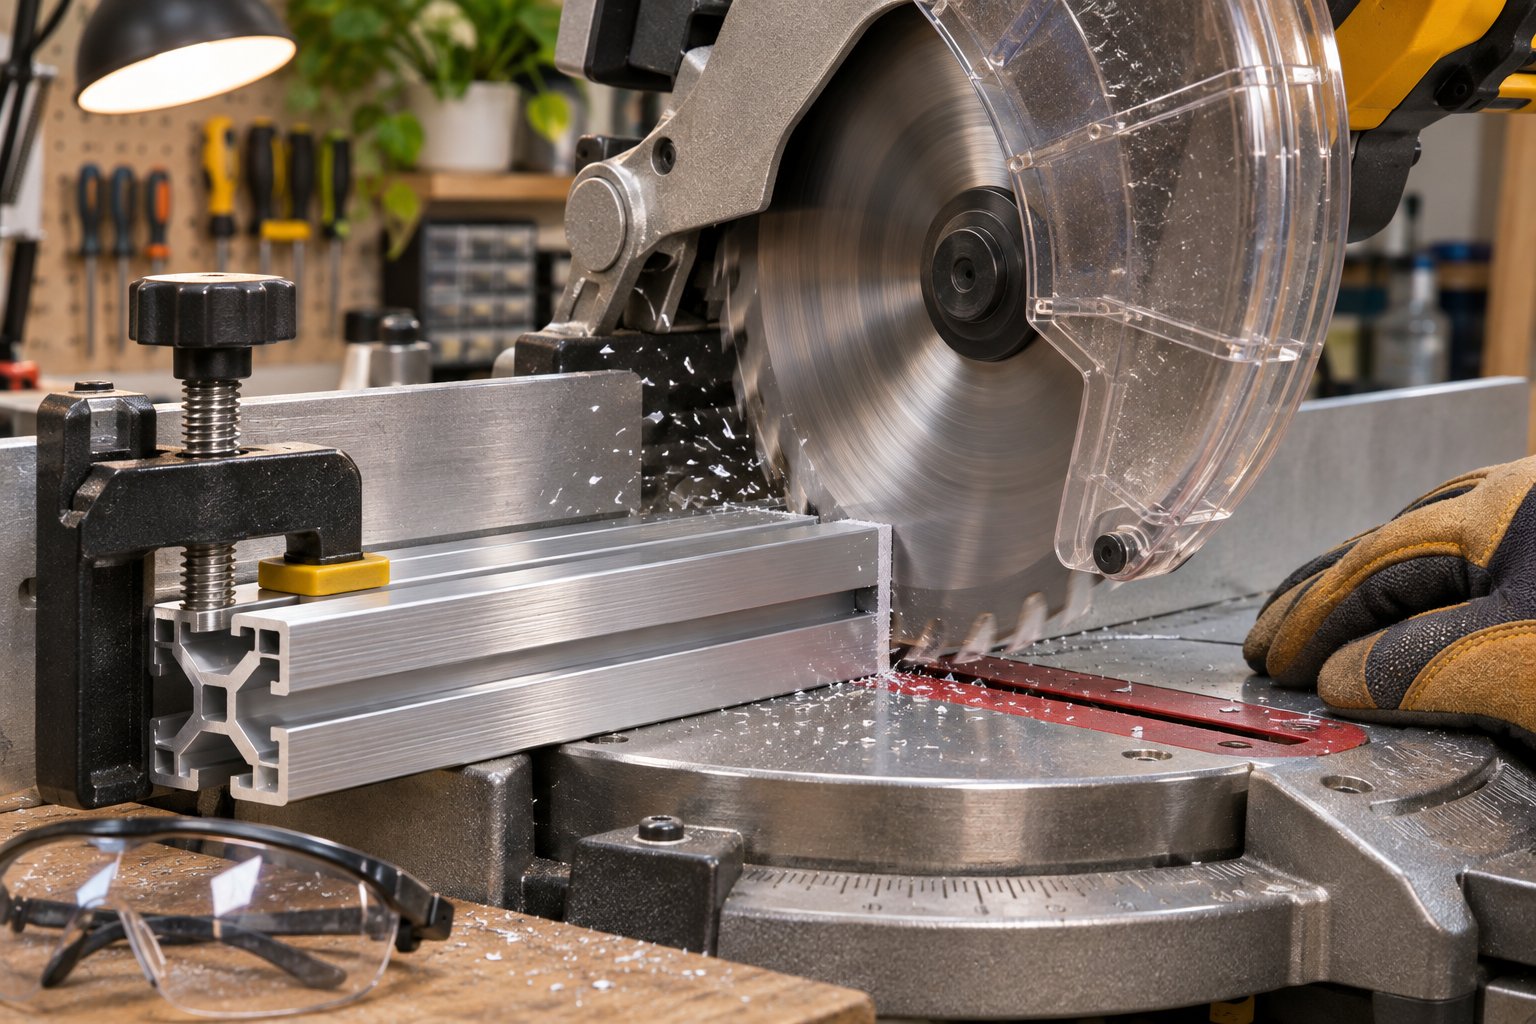
What if your frame needs a 600 mm rail and the stock comes in 1,500 mm lengths? Or a connector calls for an access hole? You can make most cuts and holes in t-slot aluminum in a home shop, often with tools you already own. A clean result depends on three things: the blade, the speed, and the cleanup afterward.
A miter saw gives the cleanest, squarest cut. Fit it with a carbide-tipped blade made for non-ferrous metal. FS Fab recommends 60 to 100 teeth for burr-free cuts in aluminum. Look for a negative hook angle. It keeps the teeth from grabbing the profile and pulling it into the blade. A carbide wood blade with an aggressive hook is the wrong choice.
Two other tools also work. A bandsaw with a bi-metal blade cuts more slowly, but it builds up little heat. A handheld circular saw with a non-ferrous blade is useful for long lengths that won't fit on a miter saw stand.
Rub stick wax or cutting lubricant on the blade before you cut. It reduces heat and keeps aluminum from sticking to the teeth, which is a main cause of burrs. Clamp the profile to the fence and table close to the cut line, because the thin walls around the slots vibrate when they're unsupported. Keep the feed steady and don't force the blade.
The saw throws hot, sharp chips instead of fine sawdust. Wear safety glasses, keep the blade guard in place, and put up a chip guard or shop curtain so the chips don't scatter.
Aluminum drills best at higher speeds than steel. Norseman Drill lists 200 to 300 surface feet per minute (SFM) for aluminum alloys and 80 to 110 SFM for steel. The tap drill for a 1/4-20 thread is a #7 bit (0.201 in.), and at 250 SFM it should turn about 4,750 RPM. Most handheld drills top out between 2,500 and 3,000 RPM. They still work if you ease off the feed pressure and use lubricant. Center punch every mark first, because the dimple stops the bit from skating across the smooth surface. A drill press keeps the hole square to the face.
For through-holes in 6063, thread with a spiral-point tap. It pushes chips ahead of the tap and out the far side, so they don't pack into the flutes. Use a cutting fluid made for aluminum, and back the tap out every so often to break the chips. Before you choose a thread, check the wall thickness, because it varies a lot across aluminum extrusion sizes. Shengxin's tapping guide puts the side walls of a 2020 profile at 1.5 to 2.0 mm. That limits direct threads to about M4. On a thin-walled t slot aluminum extrusion, a through-bolt into a T-nut usually holds better than a shallow tapped thread.
Deburr every hole and cut end with a countersink bit or a hand deburring tool. A burr left at a slot opening will catch T-nuts as they slide and scratch the anodized finish.
Follow this sequence for each cut:
The verify step also checks the stock itself. Sometimes two lengths from the same order measure differently across the slot, or the wall thickness changes from piece to piece. Careful shop work can't fix that. The variation started before the profile reached your bench.
Say two lengths from the same order measure differently across the slot. A better saw won't fix that, because the problem came from the supplier. Most listings for t-slot aluminum extrusions show a cross-section, a series number, and a price per foot. The details that decide whether your build goes together cleanly are rarely on that page, so you have to ask for them.
Before you compare prices, ask every supplier about these points:
Distributors sell catalog aluminum framing systems from stock. They cut pieces to length, ship quickly, and accept small orders. If you are searching where to buy 8020 aluminum extrusion for a single workstation, a distributor is usually the right choice. Manufacturers extrude profiles to order. For volume buyers, buying direct can lower the cost per kilogram, but minimum orders are higher and lead times are longer. US importers should compare landed cost instead of the factory price. Section 232 adds a duty of up to 50% on imported aluminum extrusions, and extrusions from China also carry antidumping and countervailing duties.
Equipment builders who plan to buy direct can use a manufacturer listing such as Shengxin Aluminium's 2020 T-track and V-slot profile to start an inquiry. The anodized finish is a good sign for slot wear and corrosion resistance. The listing has no detailed slot drawing and no hardware compatibility chart, though. Ask for both before you specify the profile, and check that your T-bolts, clamps, rollers, and fixtures fit.
Ask for a short sample length before you place a bulk order. Fit your actual T-nuts, bolts, and brackets into it, along with any rollers or jig clamps you plan to use. Slide each part along the full length of the sample. Then measure the slot opening and the cavity depth with calipers. Slot dimensions differ between manufacturers even within the same nominal series. Labels like t-rails or tslots tell you nothing about those dimensions. The same check applies to a simple aluminum t channel for a router table.
When you send the formal request for quote, list the alloy, temper, cut length and tolerance, end squareness, deburring requirement, finish, quantity, and packaging. Anything you leave out, the supplier decides for you.
Test the slot with your own hardware before you order in bulk, whatever the catalog says.
An aluminium T-track extrusion is a length of aluminum profile with a T-shaped channel running from end to end. The opening at the surface is narrower than the hollow space beneath it. A T-bolt or T-nut head can travel along the track but can't pull out through the top. You slide the fastener to the spot you want and tighten it, and the head clamps against the lips of the slot. You can then mount and move fences, stops, brackets, or panels without drilling, which plain U-channel or rectangular tube can't do. The fit depends on precise slot geometry. Small differences between manufacturers can make hardware bind or rattle, so check the slot dimensions before you buy.
All three have a T-shaped slot, but each does a different job. Structural T-slot framing is usually a square or rectangular bar with slots on up to four faces. The bars bolt together with T-nuts and brackets to build frames, guarding, and machine bases. V-slot profiles shape the slot edges into a V-groove so wheels can roll along them, which makes them popular for 3D printers and hobby CNC gantries. Dedicated T-track is a slim single-channel strip set into a workbench, router table, or sled to lock jigs and clamps. It is not meant to carry structural loads. Some profiles combine features, such as Shengxin Aluminium's anodized 2020 T-track and V-slot extrusion. Its listing has no slot drawing or hardware compatibility chart, so test your T-bolts, clamps, and rollers before you specify it.
No. Inch (fractional) and metric series use different slot widths and cavity shapes, so their T-nuts and brackets don't fit each other's profiles. For example, 10 series inch profiles have a slot of about 0.26 in., while 20 mm metric profiles use a 6 mm slot. The numbers look close, but the hardware still won't seat properly. Even within one series, slot depth and flange thickness can vary between brands. Pick one system at the start of the project, get the profile drawing, and check it against your fastener datasheets. When you buy from a new supplier, order a short sample first and slide your actual hardware along its full length.
For most framing, fixtures, and woodworking track, 6063-T5 is the better choice. It flows easily through extrusion dies, so slot details stay crisp, it anodizes cleanly, and it resists corrosion very well. 6061-T6 is stronger, with a yield strength of about 276 MPa against about 214 MPa for 6063, and it handles fatigue better. That makes it the choice for frames under heavy, vibrating, or impact loads. The downsides are higher cost and fine features that are harder to hold. 6105-T5 falls between the two. All three alloys flex about the same for a given shape, because stiffness comes mainly from the cross-section and wall thickness. Compare the full profile specification, not just the alloy.
A miter saw with a carbide non-ferrous blade gives the squarest cut. Choose a high tooth count, roughly 60 to 100 teeth, and a negative hook angle so the blade doesn't grab the profile. A bandsaw with a bi-metal blade or a circular saw with a non-ferrous blade also works. Wax the blade, clamp the extrusion close to the cut line, feed steadily, and wear eye protection against hot chips. For holes, center punch first, run the drill faster than you would for steel, and thread with a spiral-point tap and aluminum cutting fluid. Thin walls, such as the 1.5 to 2.0 mm sides of a 2020 profile, can't hold large threads, so a bolt into a T-nut is often stronger. Deburr every edge so T-nuts slide freely.


 خدمة الإنترنت
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 العربية
 English
 français
 Deutsch
 русский
 español
 português
 ไทย
 Việt
 Українська